Bicycle Disc Brake Components CNC Machining Case Study

This disc brake case follows a bicycle caliper and rotor interface from drawing review through machining and inspection planning. The focus is on mounting alignment, bore or fastening features and the relationship between the caliper and disc brake rotor.

Get Your Braking Quote
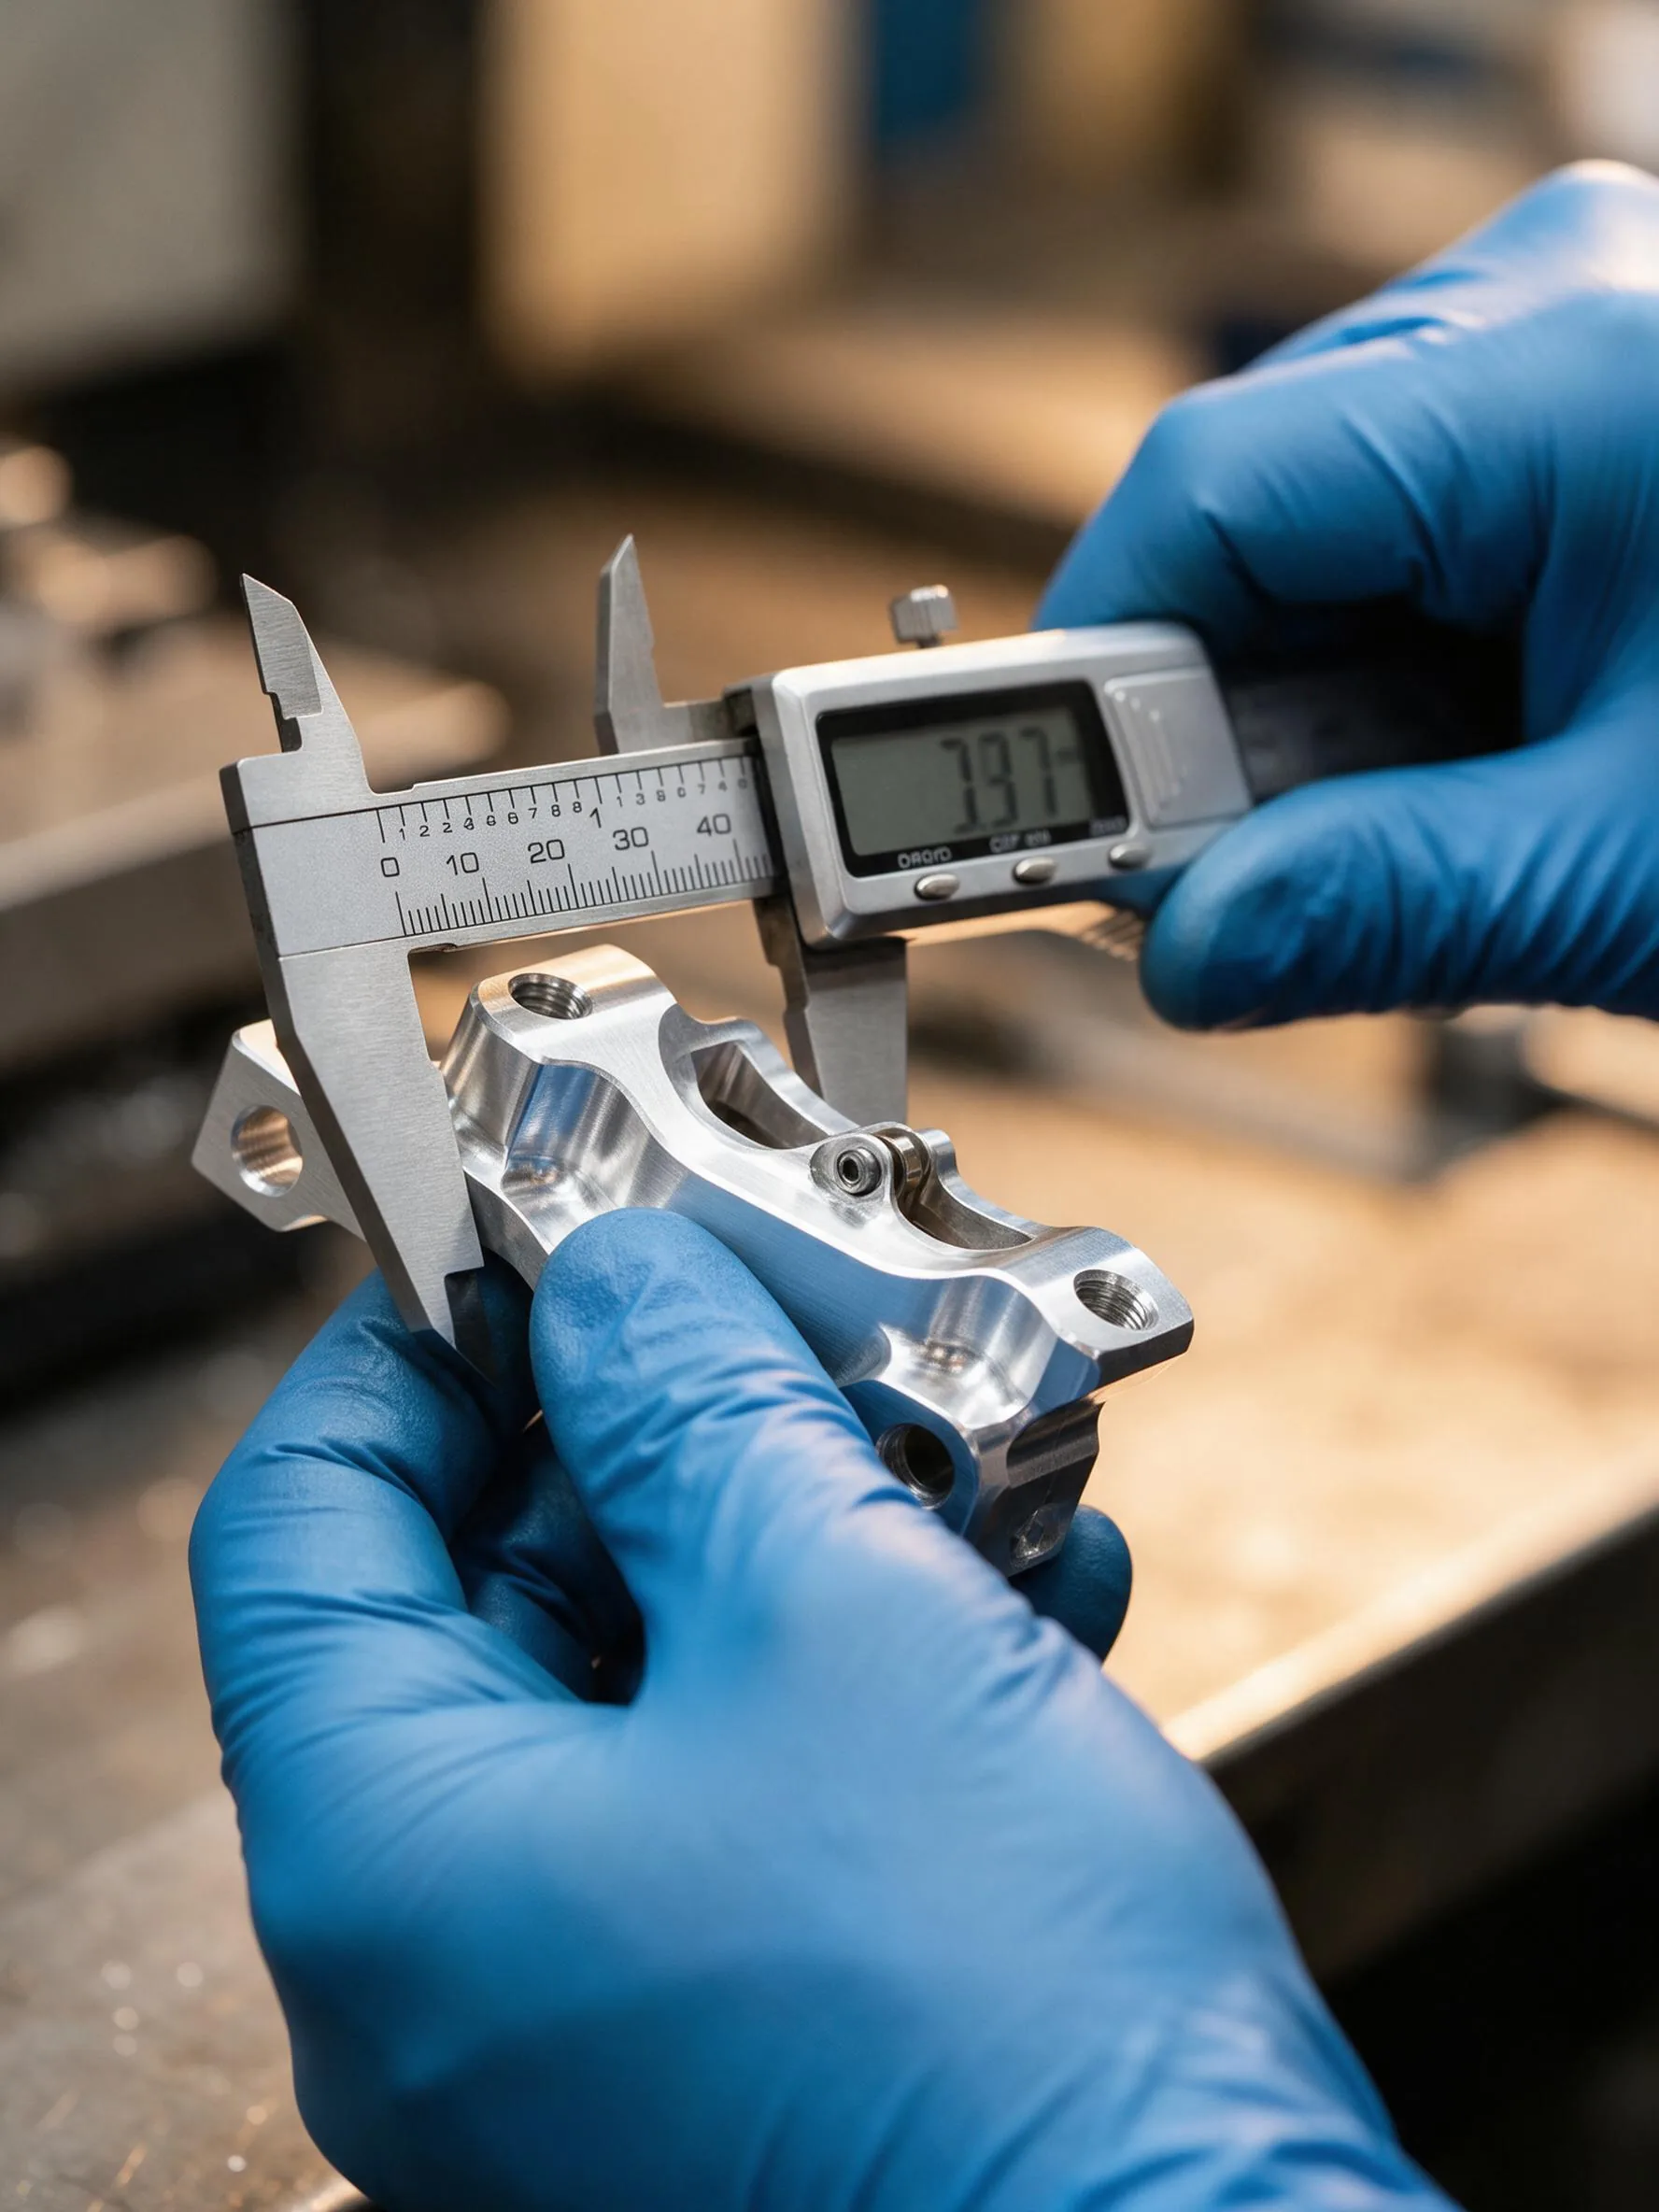
Digital caliper measuring a CNC machined 7075-T6 bicycle brake caliper
AL 7075-T6 Β· BRAKE CALIPER

Case Brief: Part Function and Requirements

The case centers on bicycle disc brake components where the caliper, adapter and rotor must locate consistently on the fork or frame. A disc brake rotor and bicycle disc brake caliper are considered together so the scope reflects the actual bicycle disc brake components and their mounting interfaces.

The process review sets datums from the mounting features, chooses workholding that exposes the critical faces and defines checks from the drawing. Disc brake inspection here means dimensional verification of machined interfaces; it is not a maintenance guide or a claim about braking performance.

Hydraulic Calipers Disc Rotors Master Cylinders Brake Levers Adapters 5-Axis Machining
Start Your Braking Project

Manufacturing Process and Setup

A brake-specific workflow engineered for pressure integrity and weight reduction.

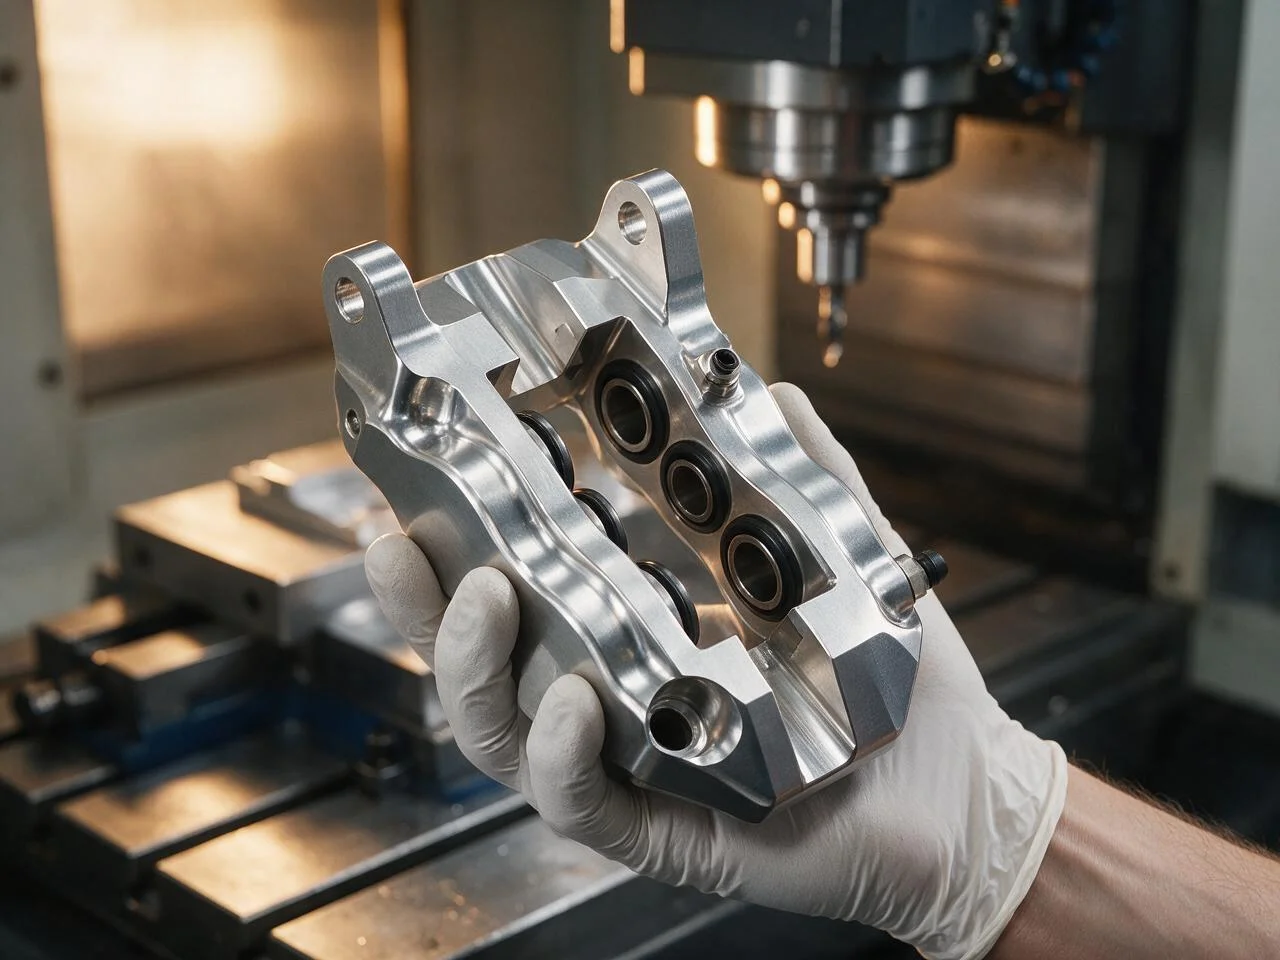
5-axis CNC machining of a bicycle hydraulic brake caliper from 7075-T6 billet
1

Housing Roughing

5-axis roughing removes bulk material from 7075-T6 billet while leaving consistent stock for finish passes.

2

Piston Bore Machining

The drawing defines the datums and fit criteria for piston bore machining; inspection scope is agreed for the project.

3

Hydraulic Passages

Cross-drilled channels are deburred and sealed; banjo and bleed ports threaded to UNF Fit requirements per drawing.

4

Seal Grooves

5

Pressure Test

Pressure-test requirements and acceptance criteria are confirmed against the customer specification for the individual project.

6

Hard Anodize

Type III anodizing provides wear resistance on piston bores and corrosion protection for the housing.

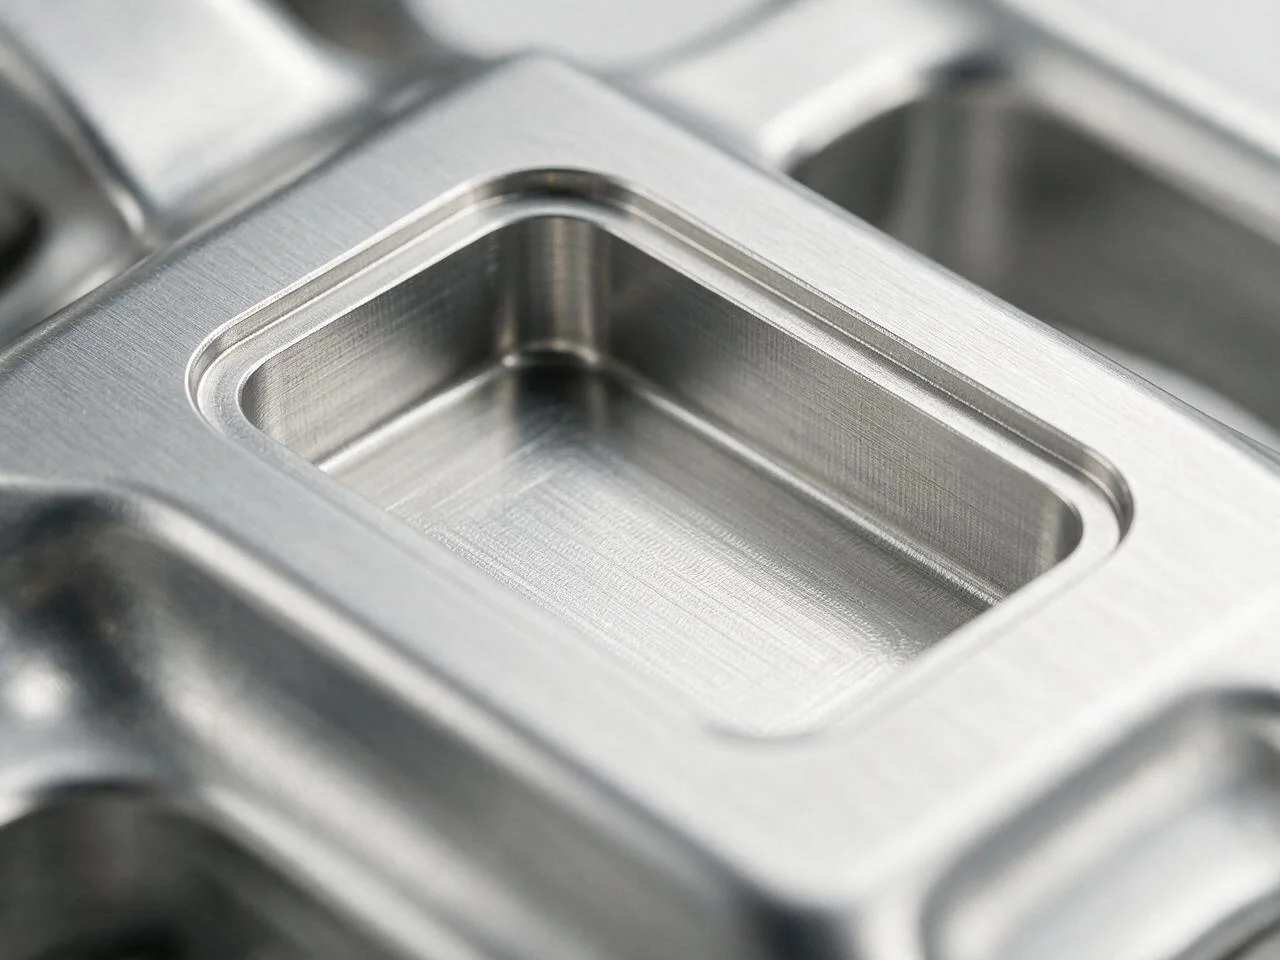
Close-up of a machined seal groove on a bicycle brake caliper body
Request Caliper Machining

Case Components and Machining Focus

Each part is engineered for hydraulic integrity, thermal management, and crash durability.

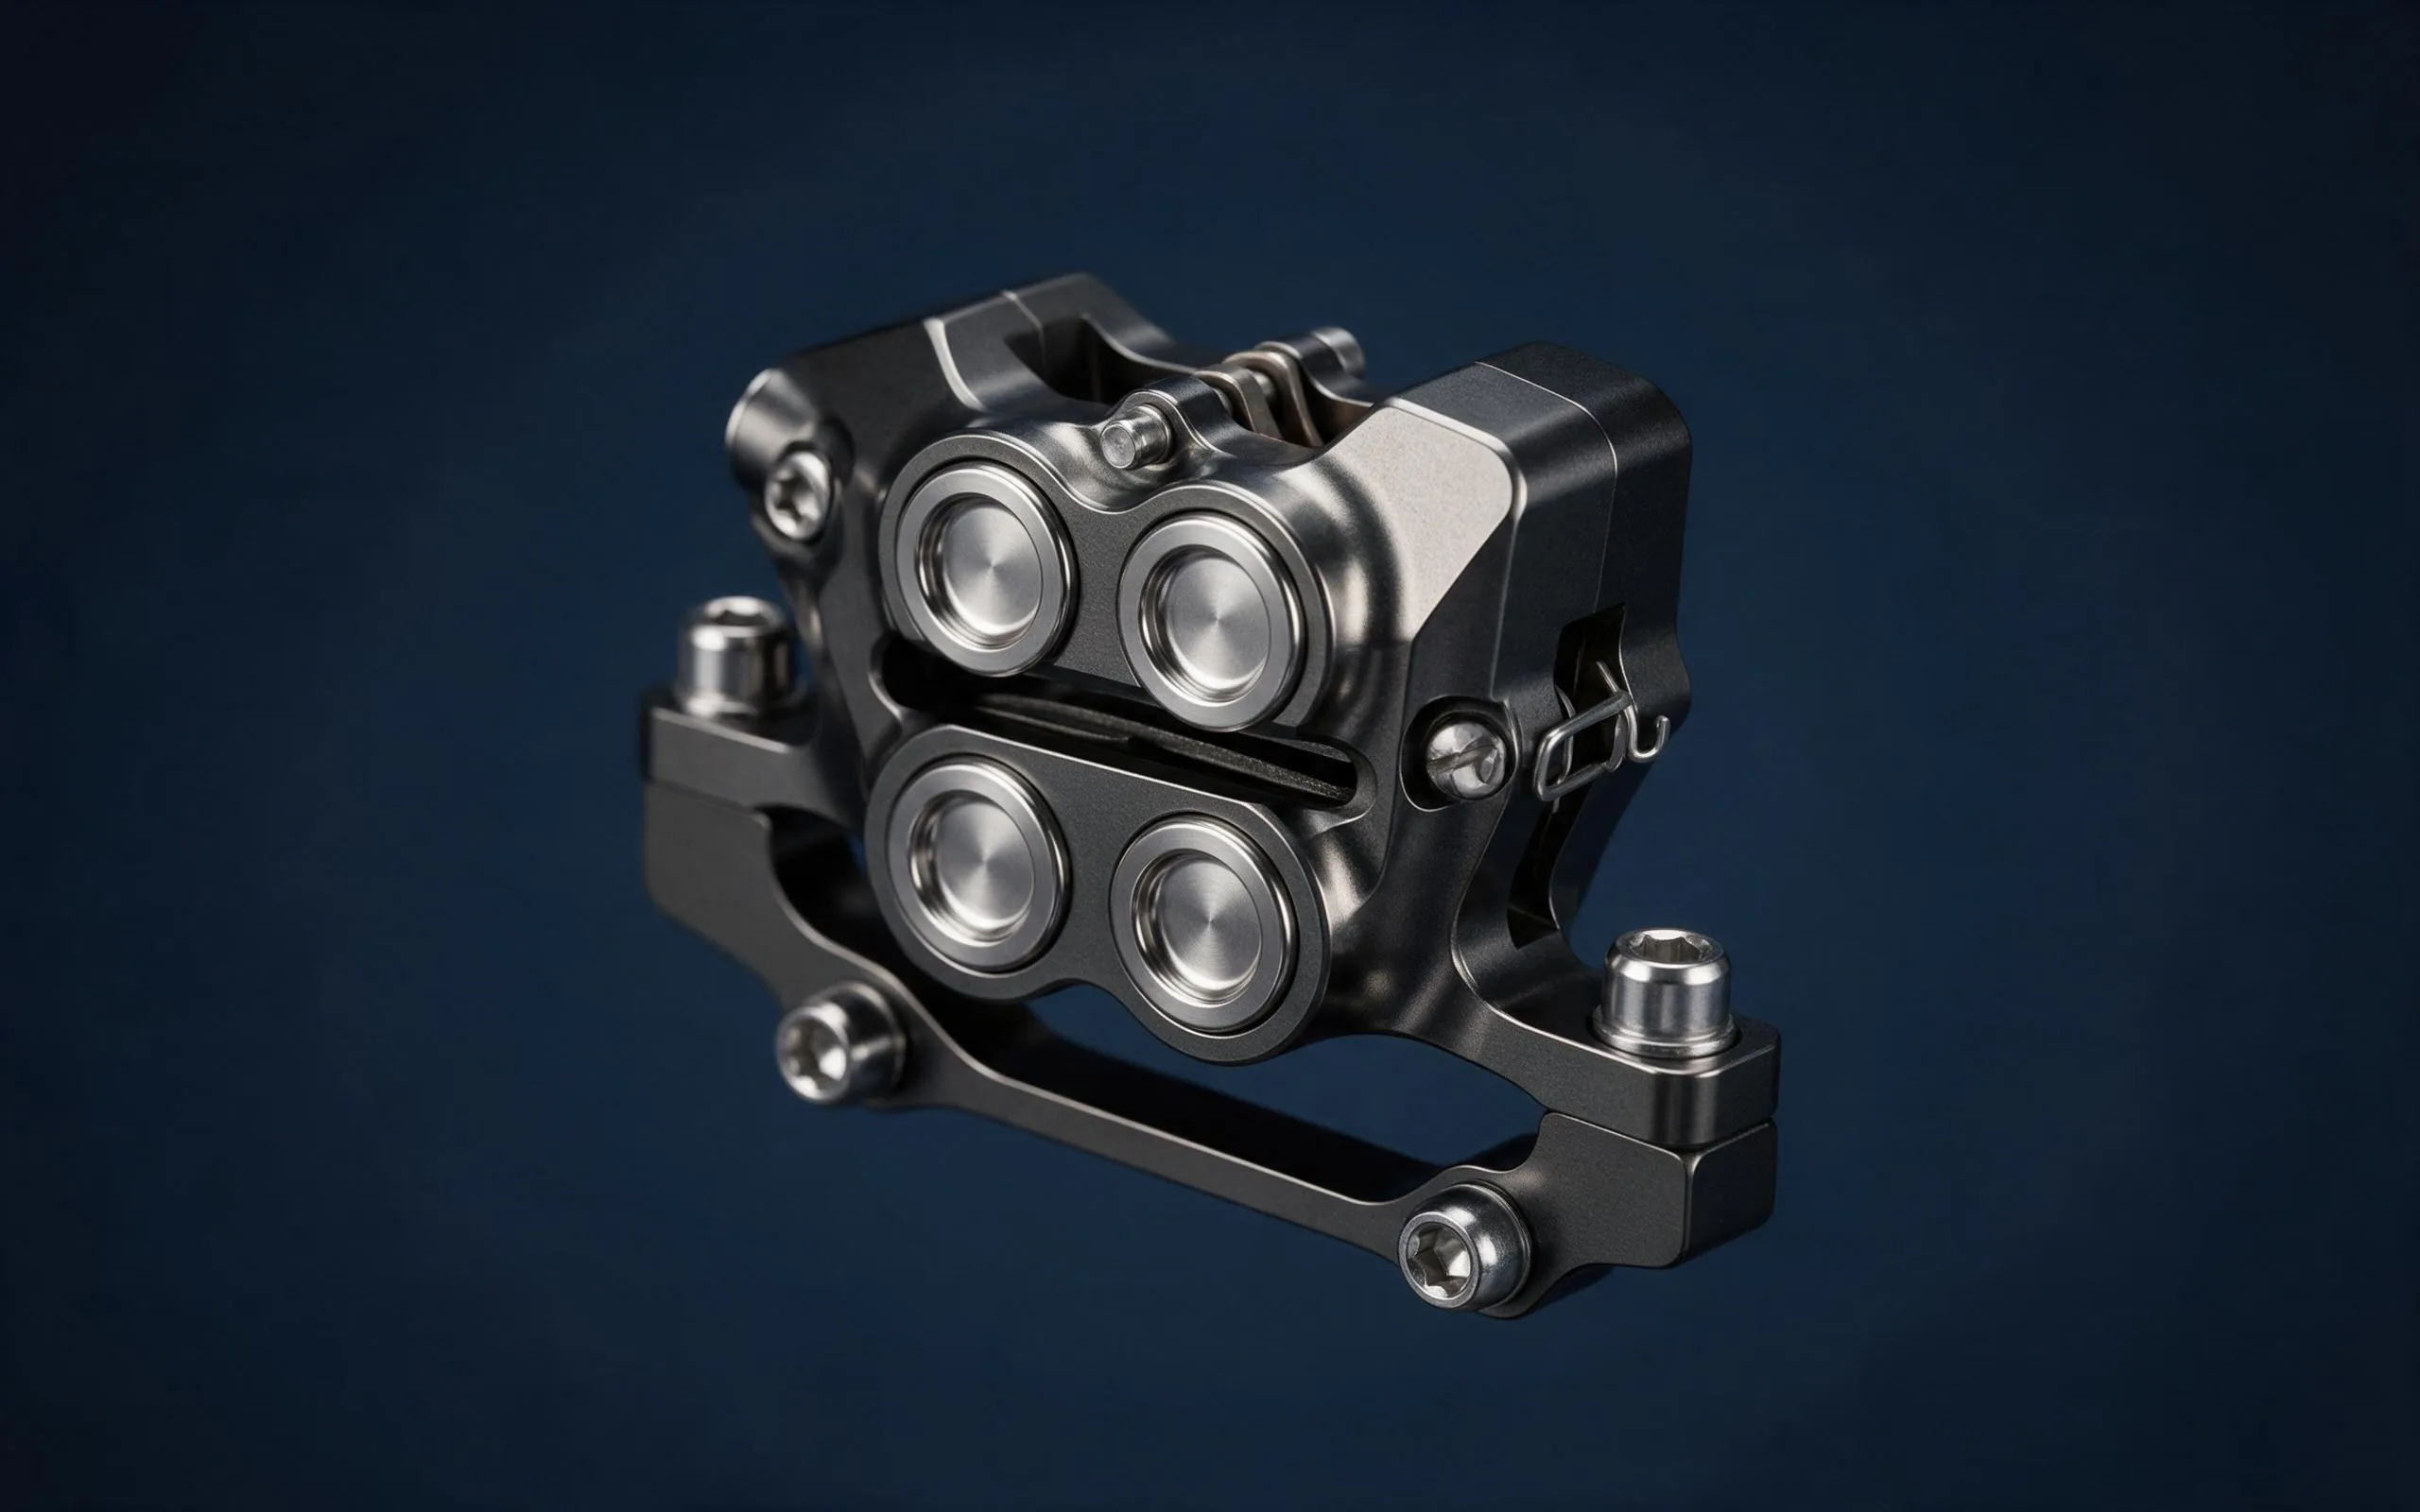
Disc Brake Calipers

2-Piston / 4-Piston

The caliper is the heart of a hydraulic disc brake. We machine two-piece and monobloc calipers from 7075-T6 aluminum, with piston bores honed to meet fit requirements on the drawing tolerance and hydraulic passages deburred to prevent seal damage. According to our CNC machining knowledge base, aluminum remains widely used for CNC machining due to excellent machinability and availability of alloys and treatments.

7075-T6 Bore fit per drawing Per drawing / agreed scope
Quote Calipers
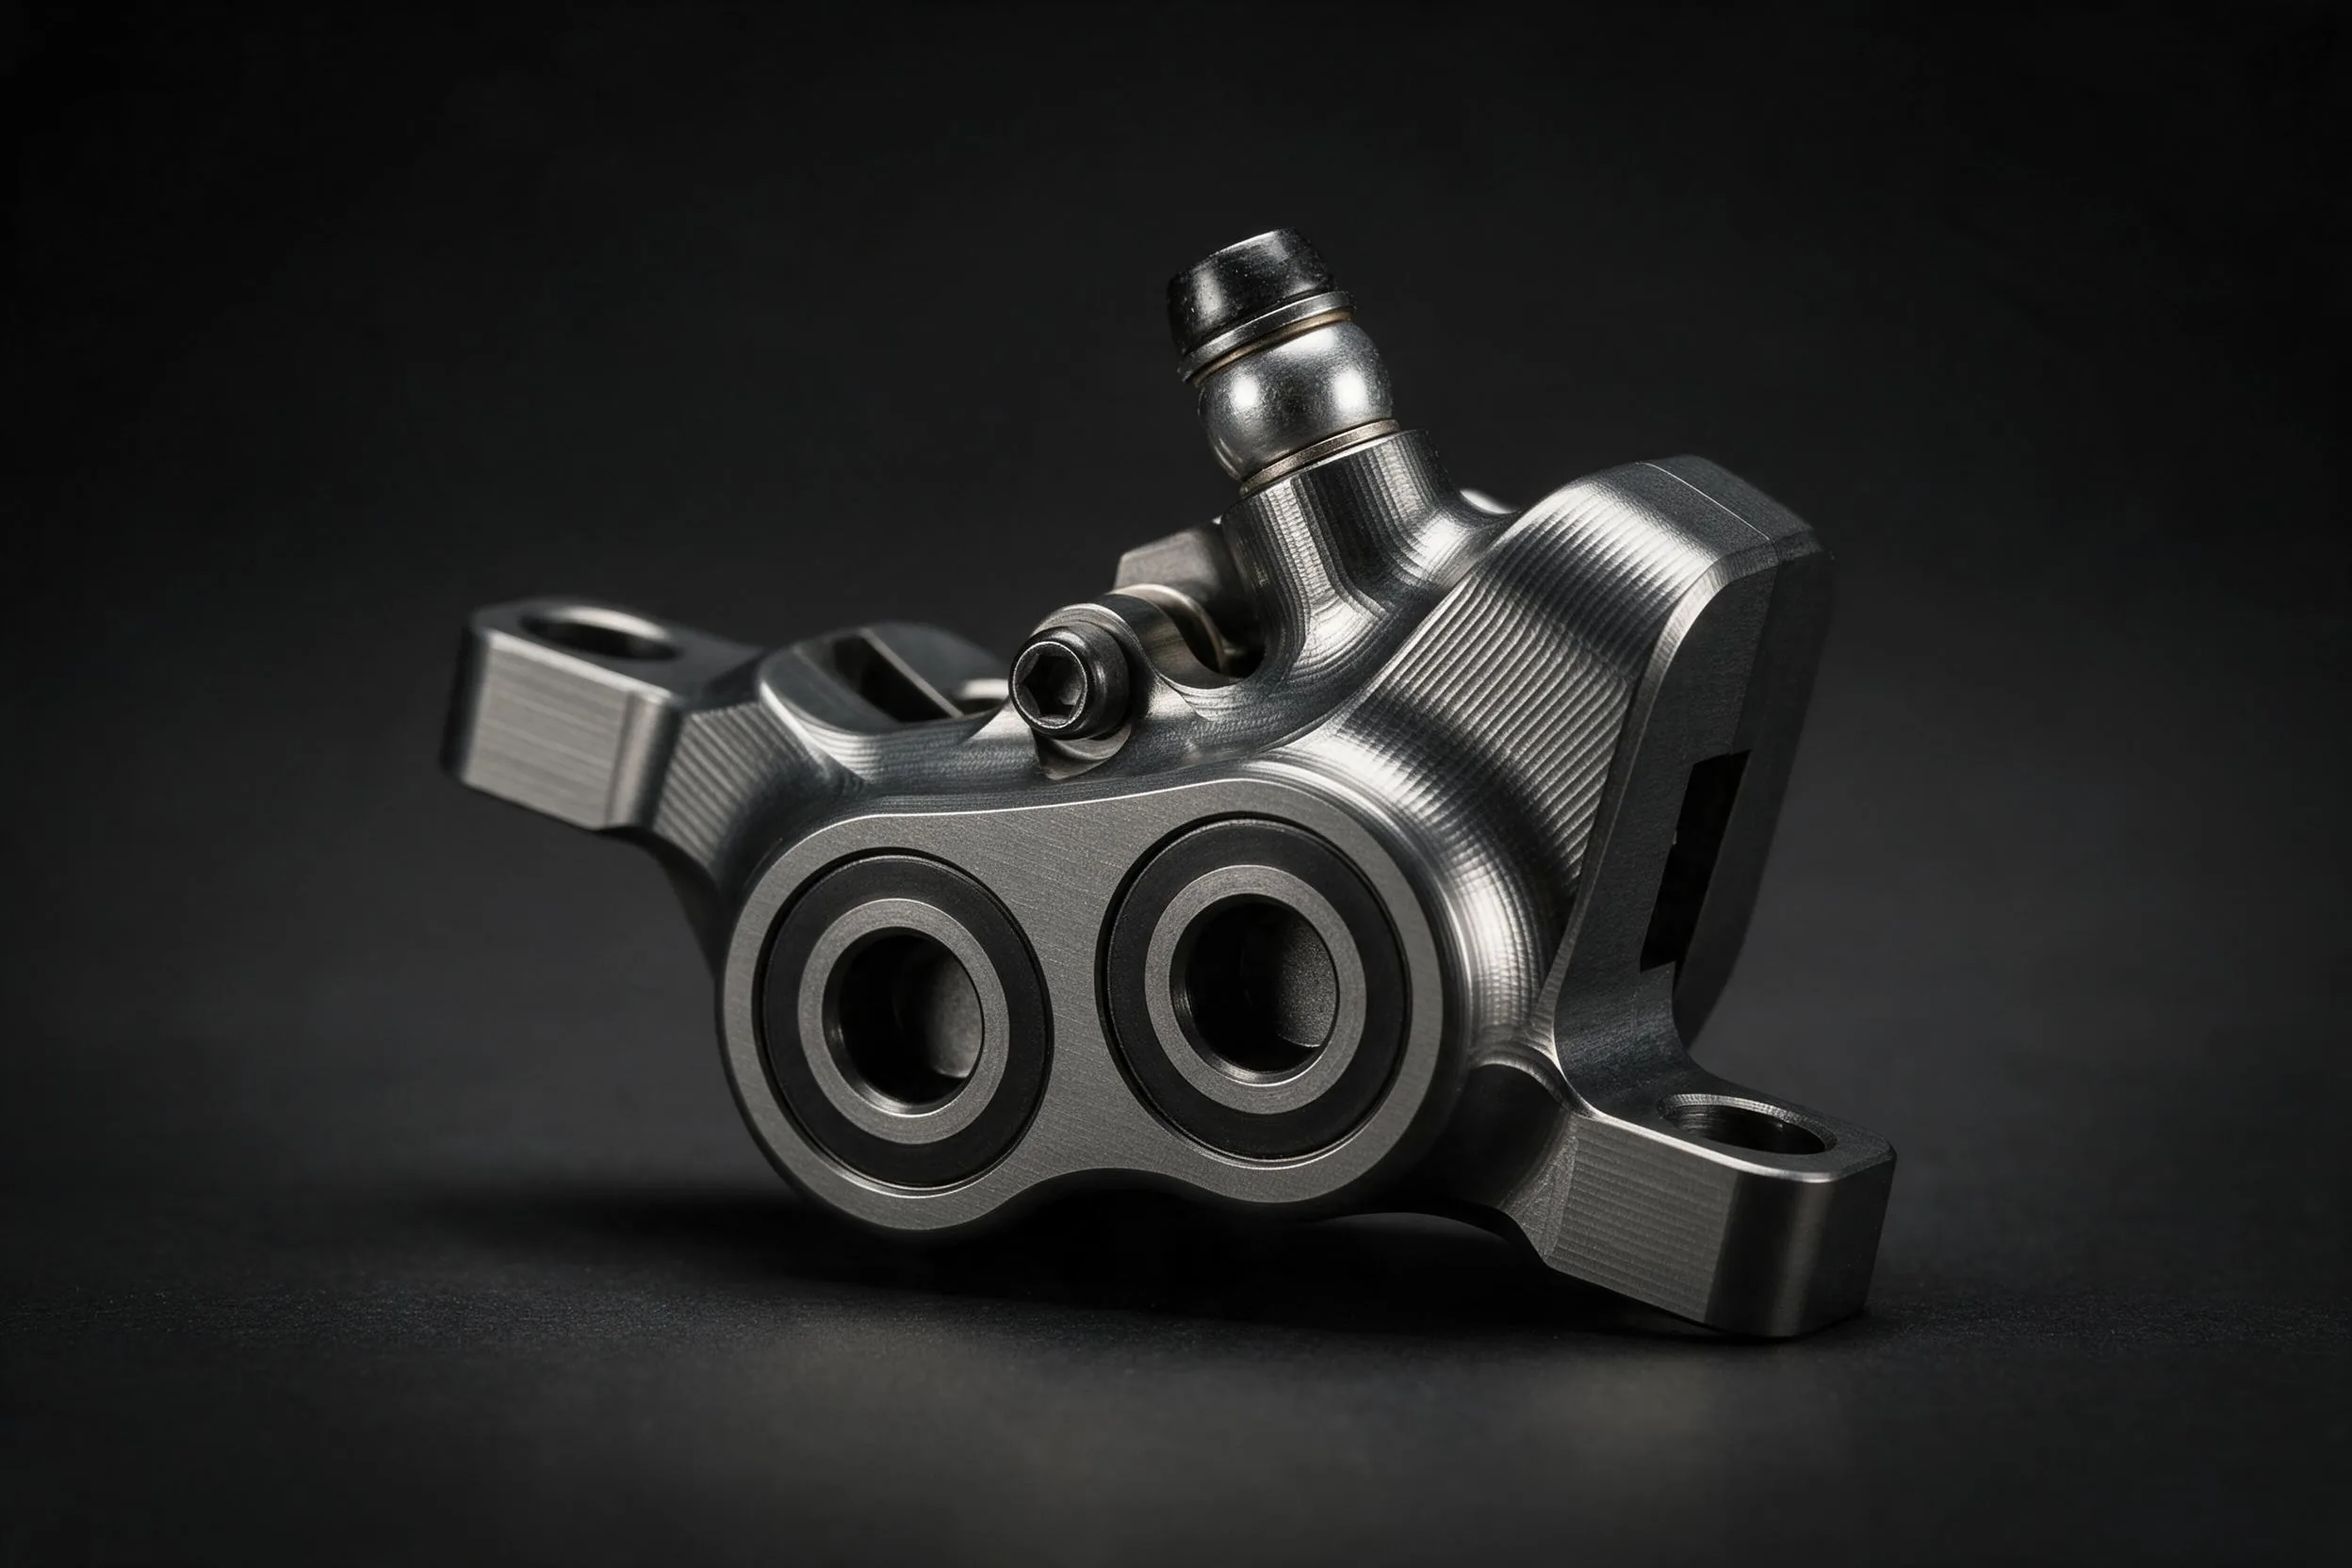
CNC machined bicycle disc brake caliper
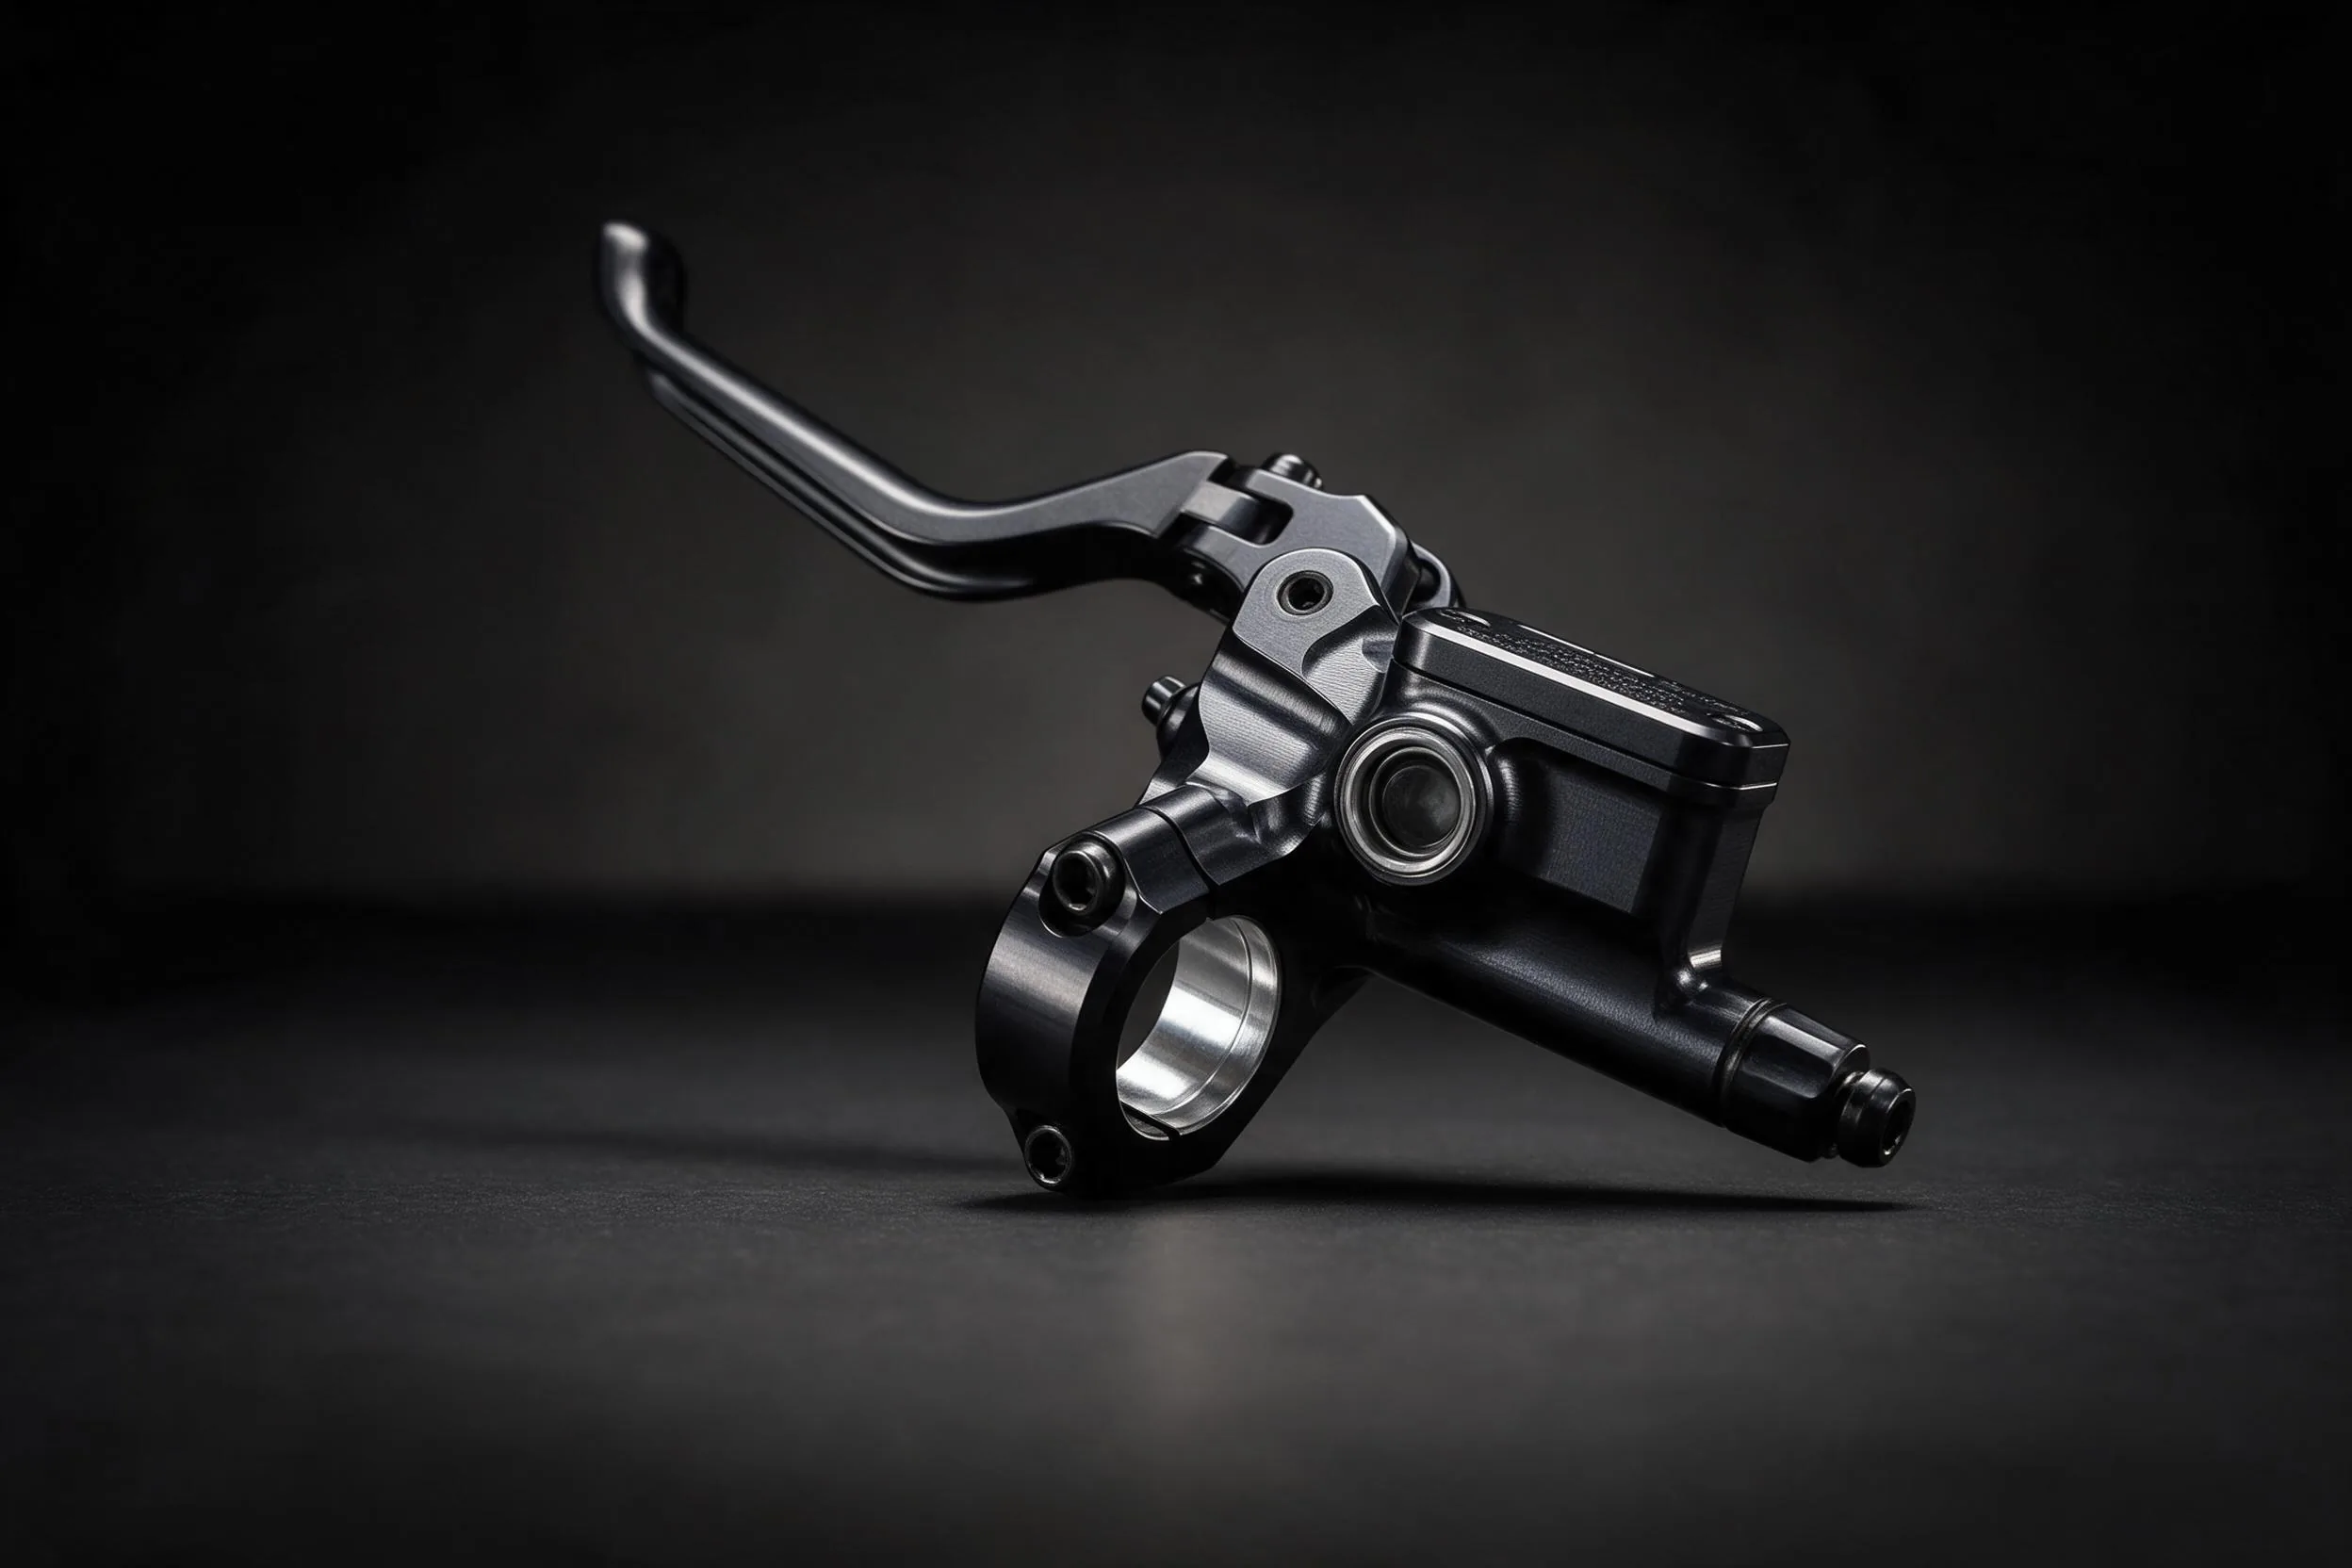
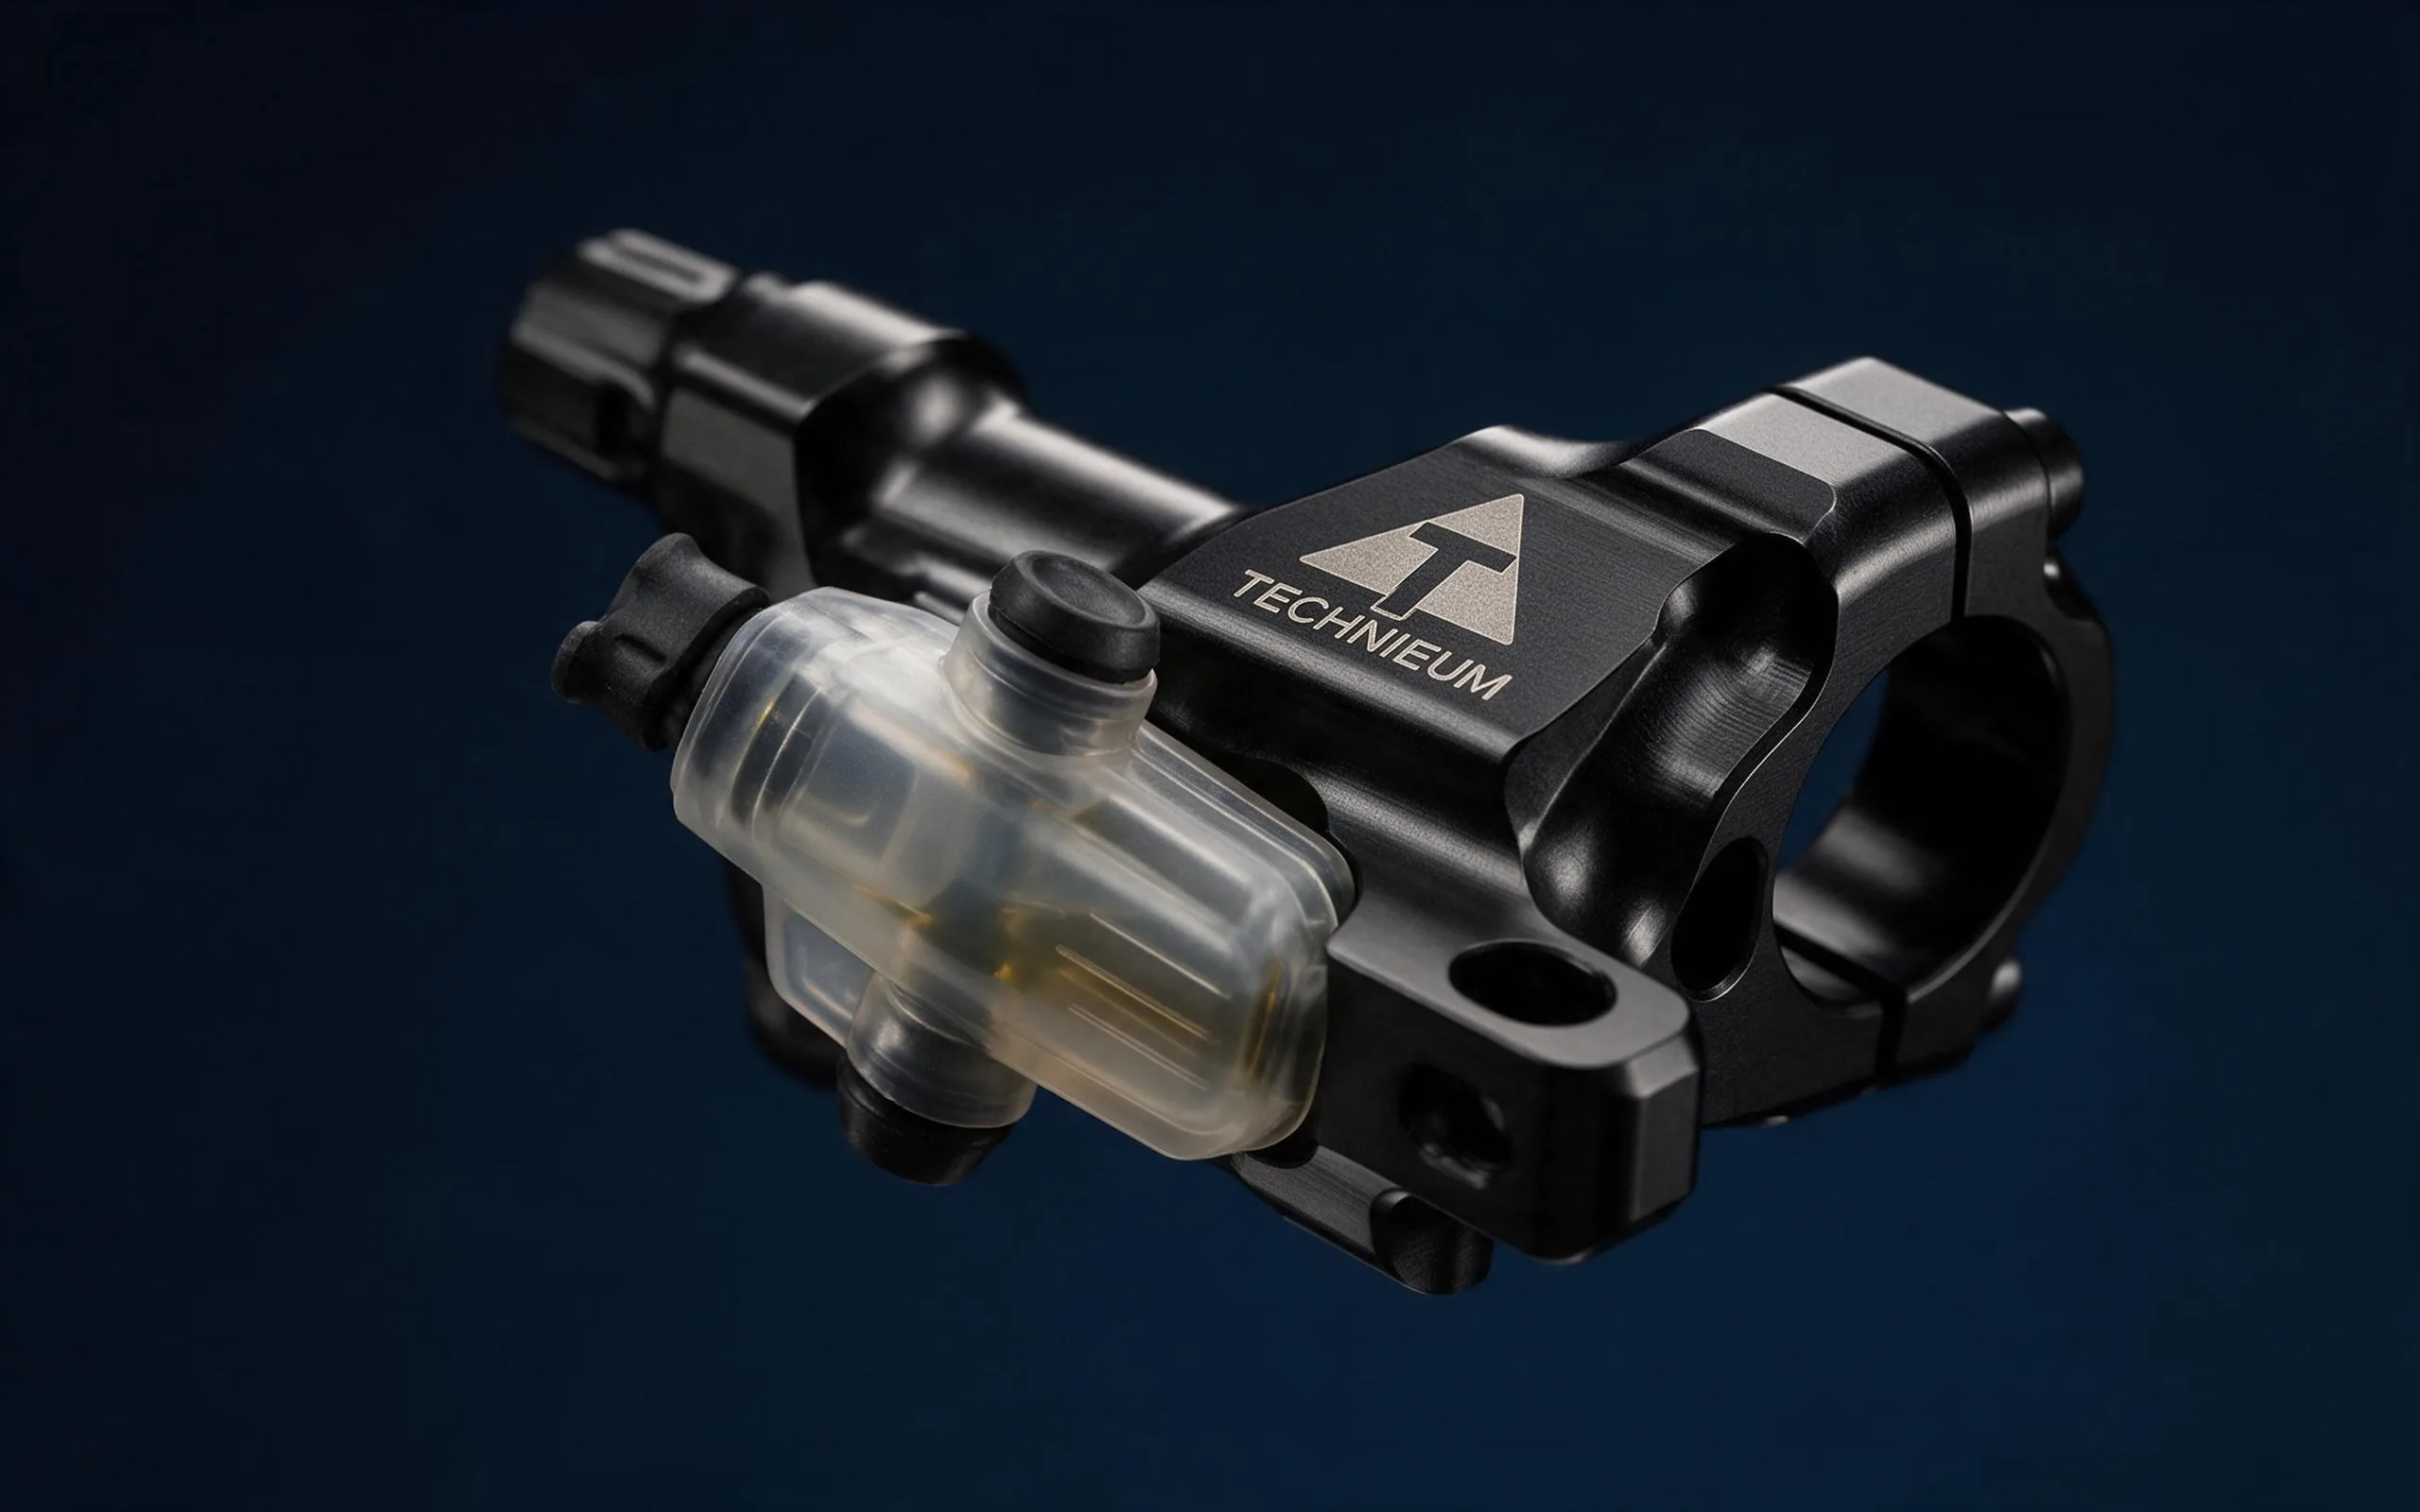
CNC machined bicycle brake master cylinder

Master Cylinders

Open / Closed System

Pressure-test requirements and acceptance criteria are confirmed against the customer specification for the individual project.

6061-T6 / 7075-T6 Per drawing / agreed scope ISO 4210
Quote Master Cylinders

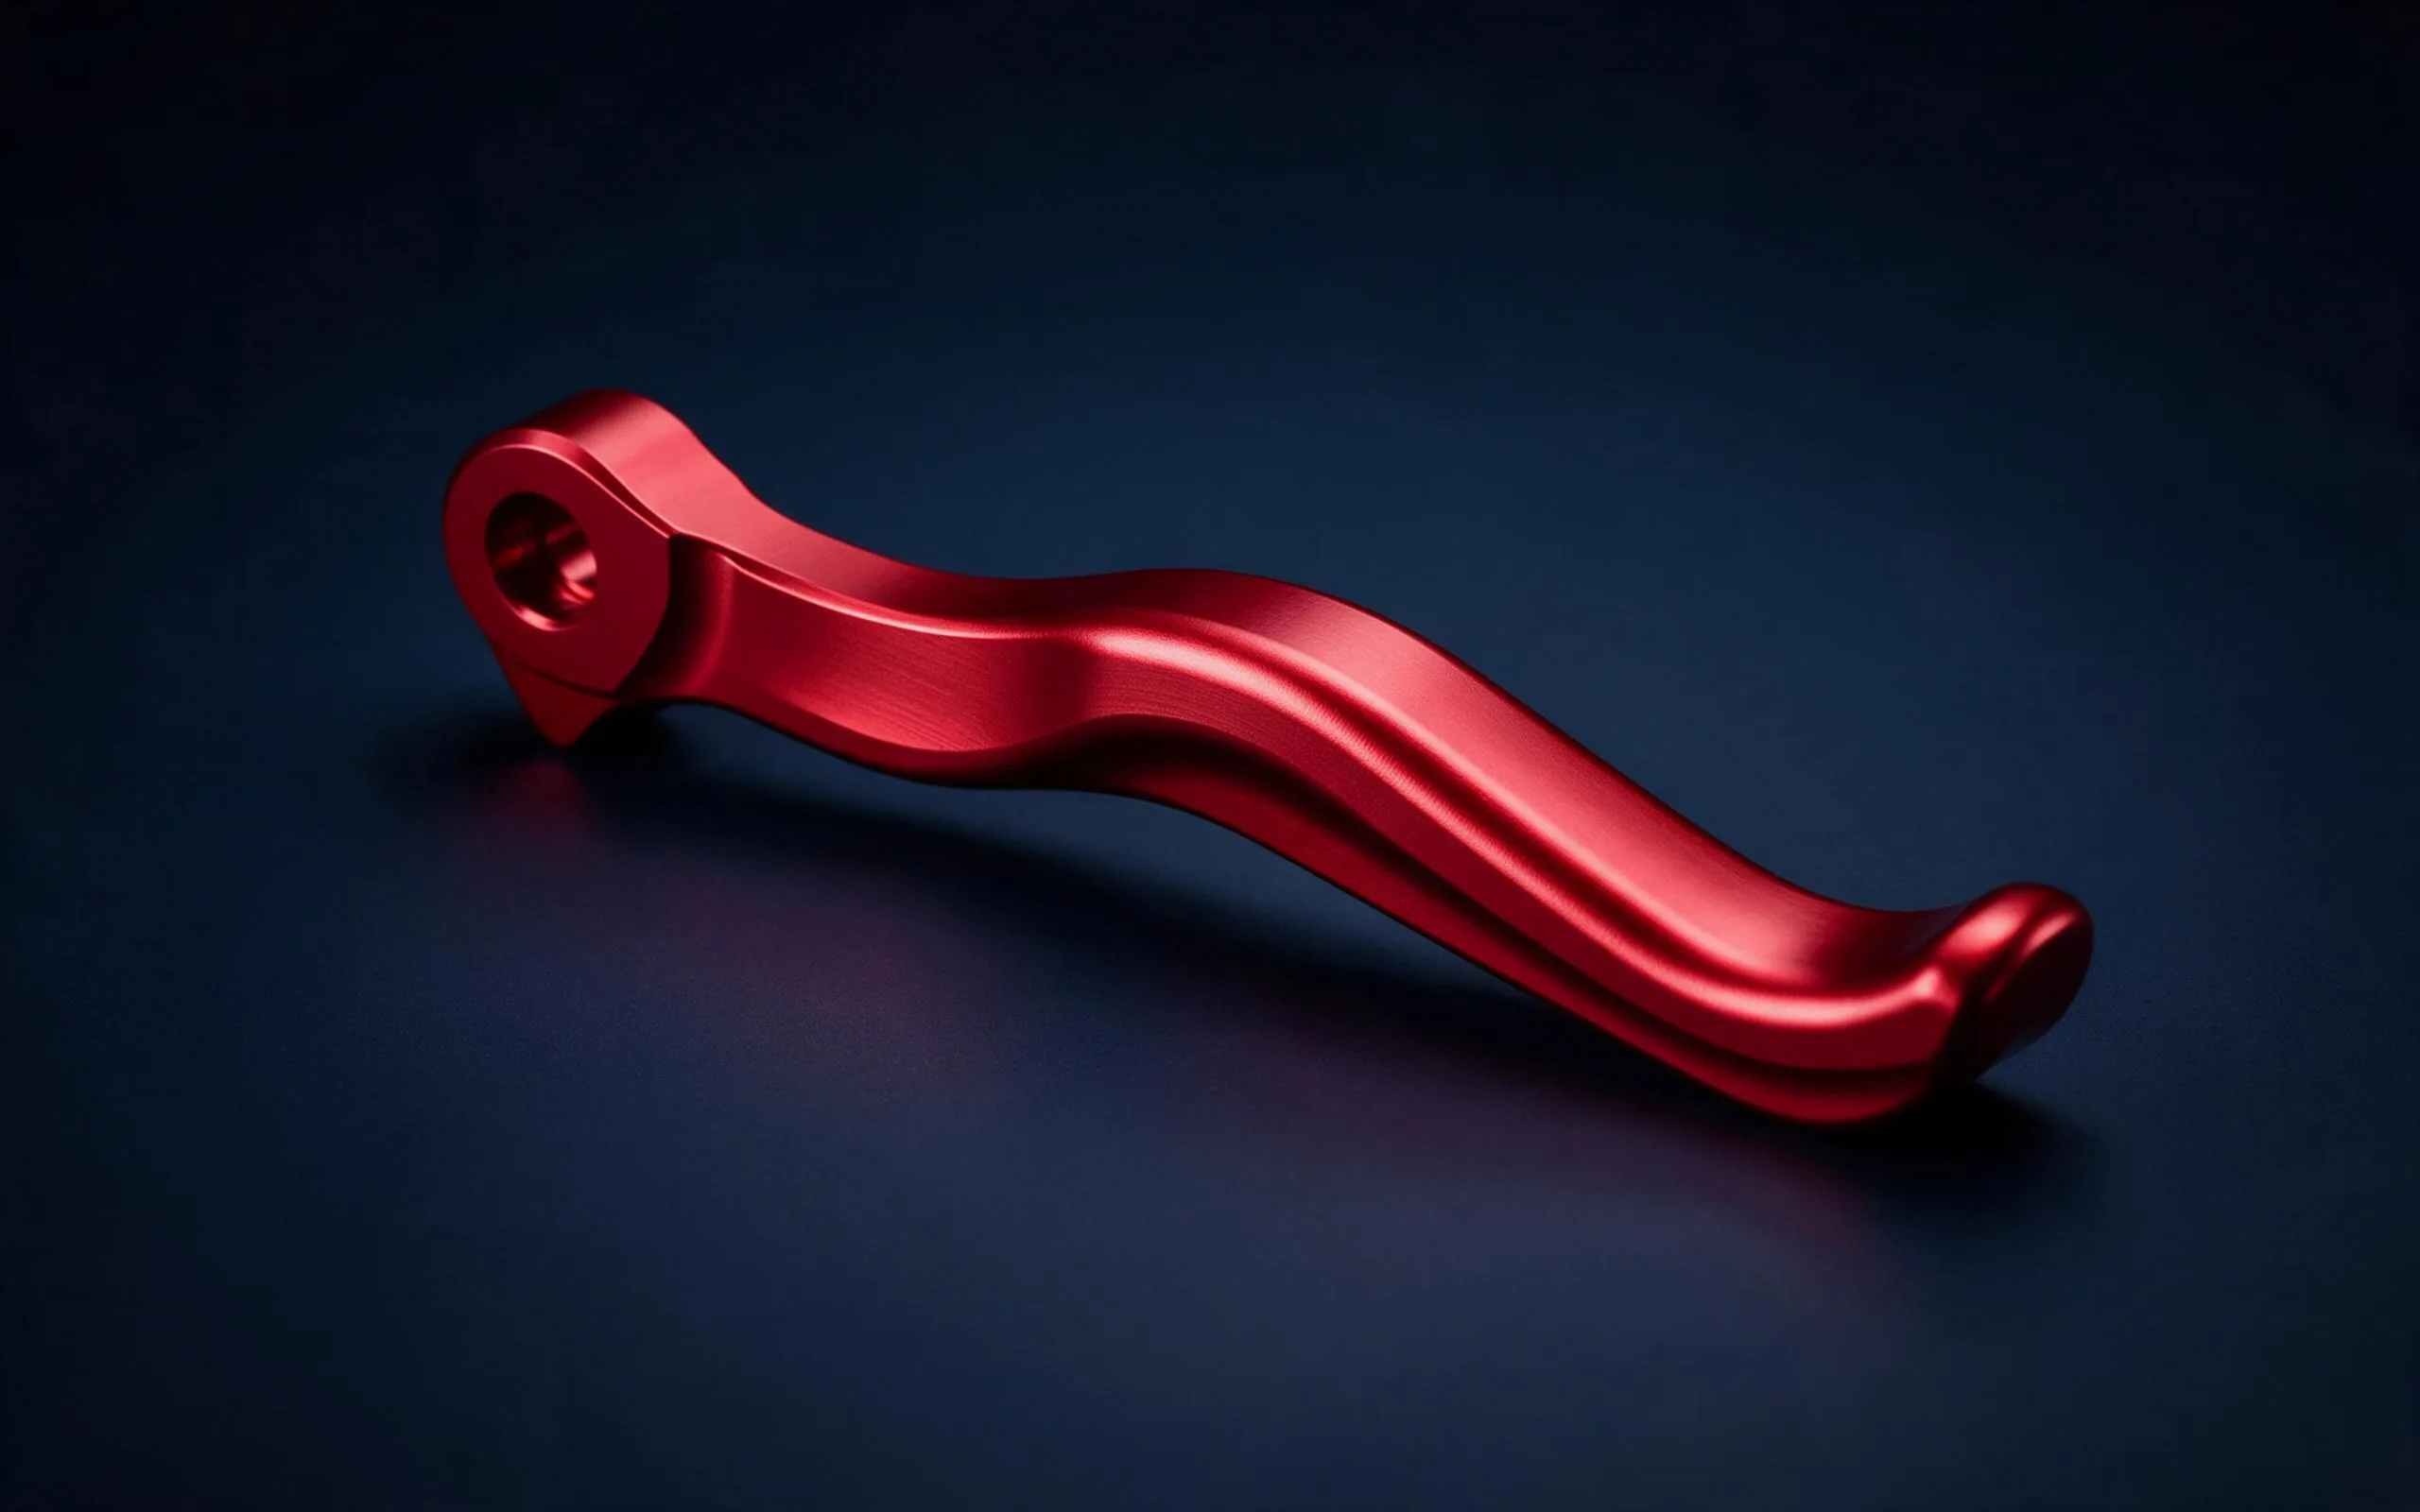
Brake Levers

Forged Billet
Al 7075-T6 Per drawing Pivot Type II Anodize
Quote Brake Levers
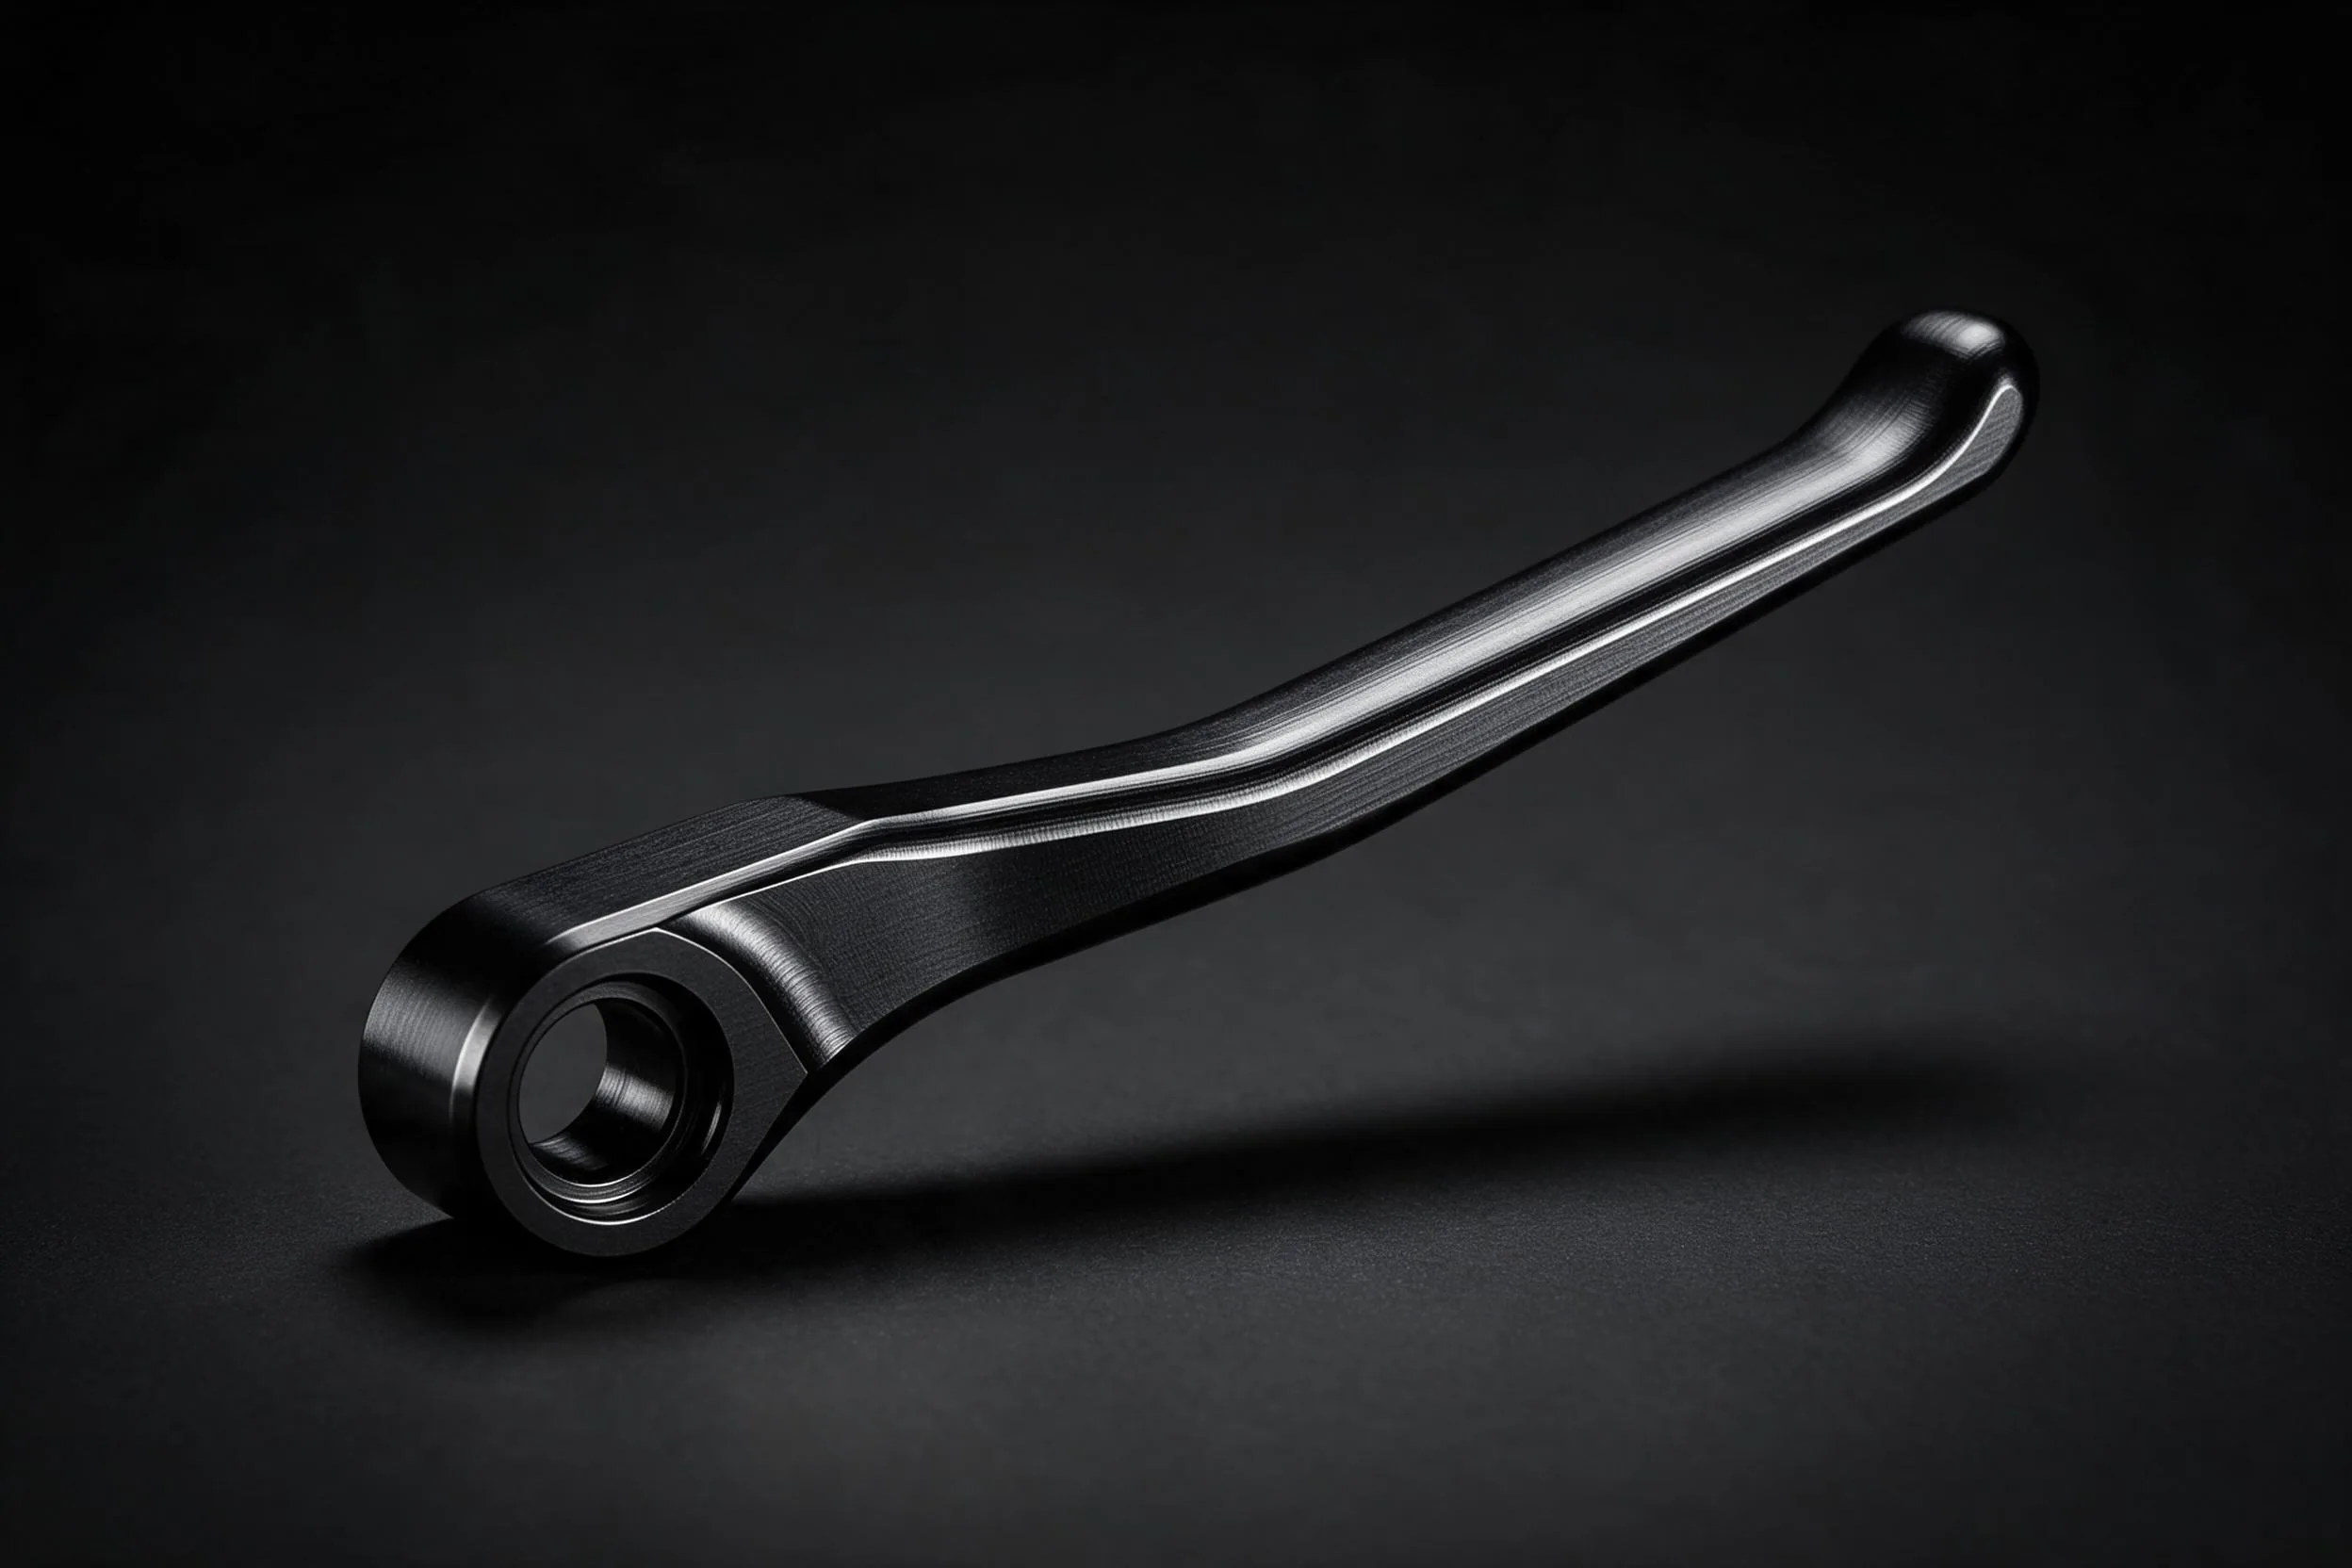
CNC machined bicycle brake lever
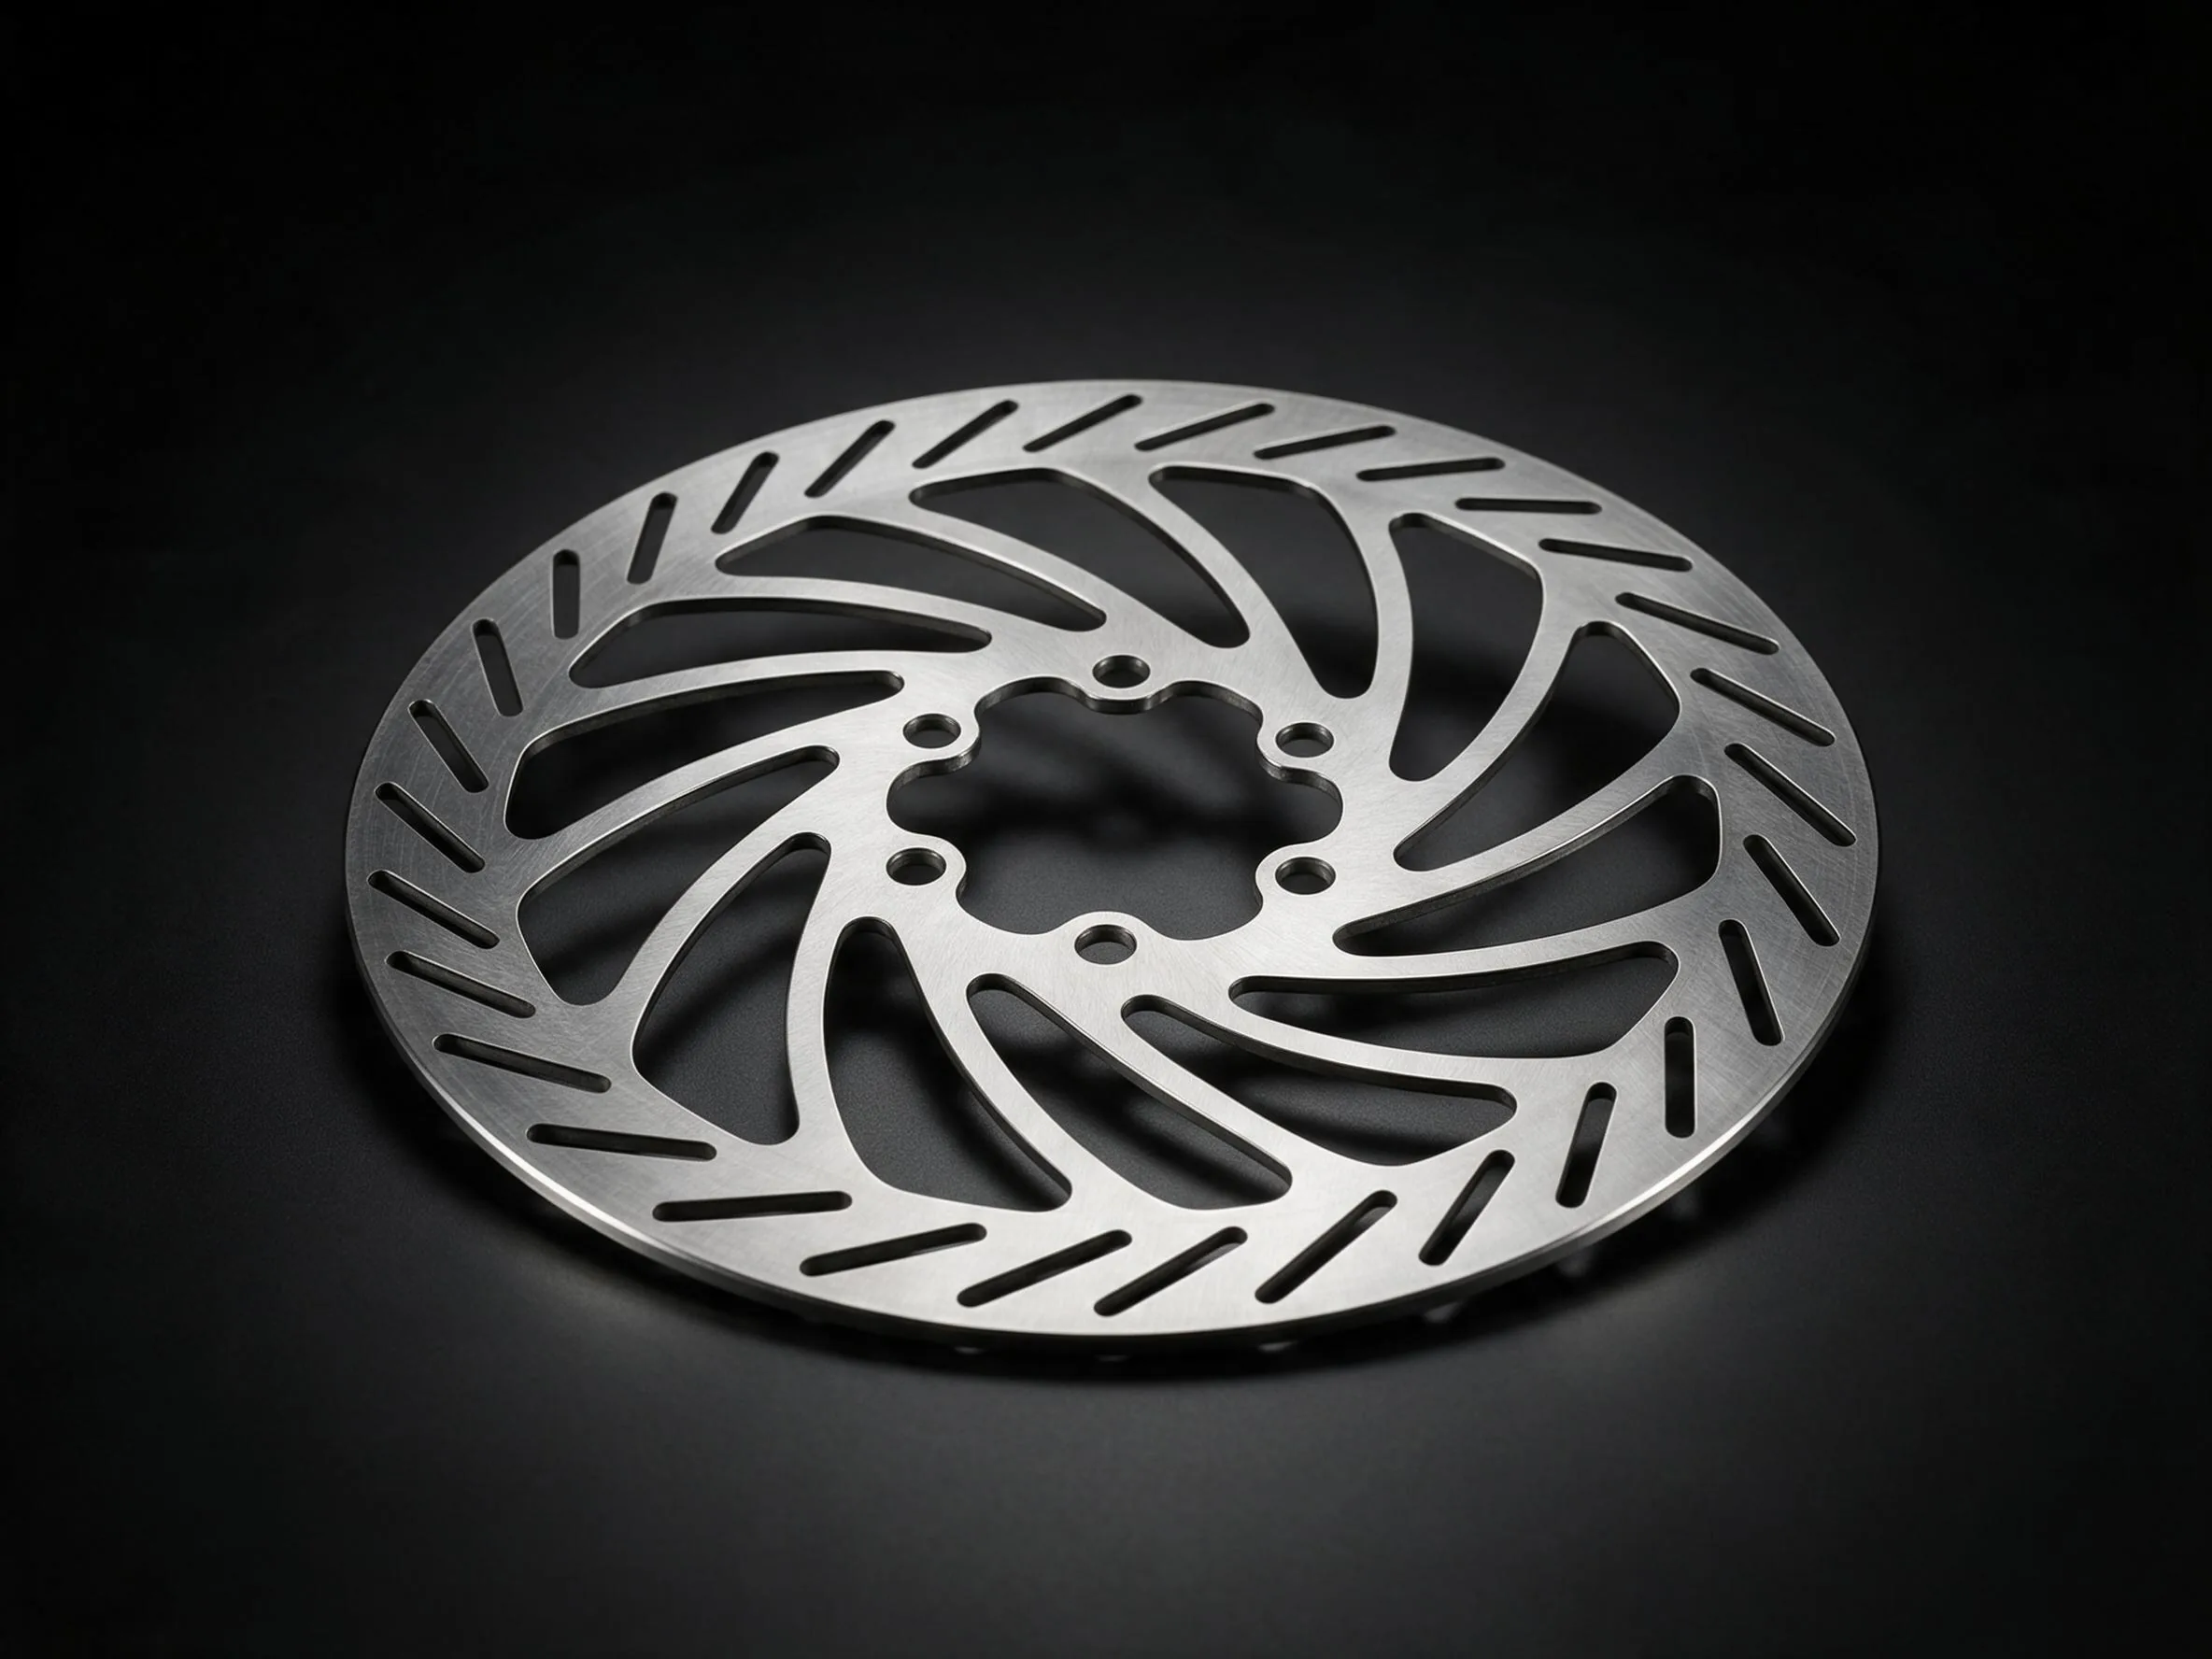
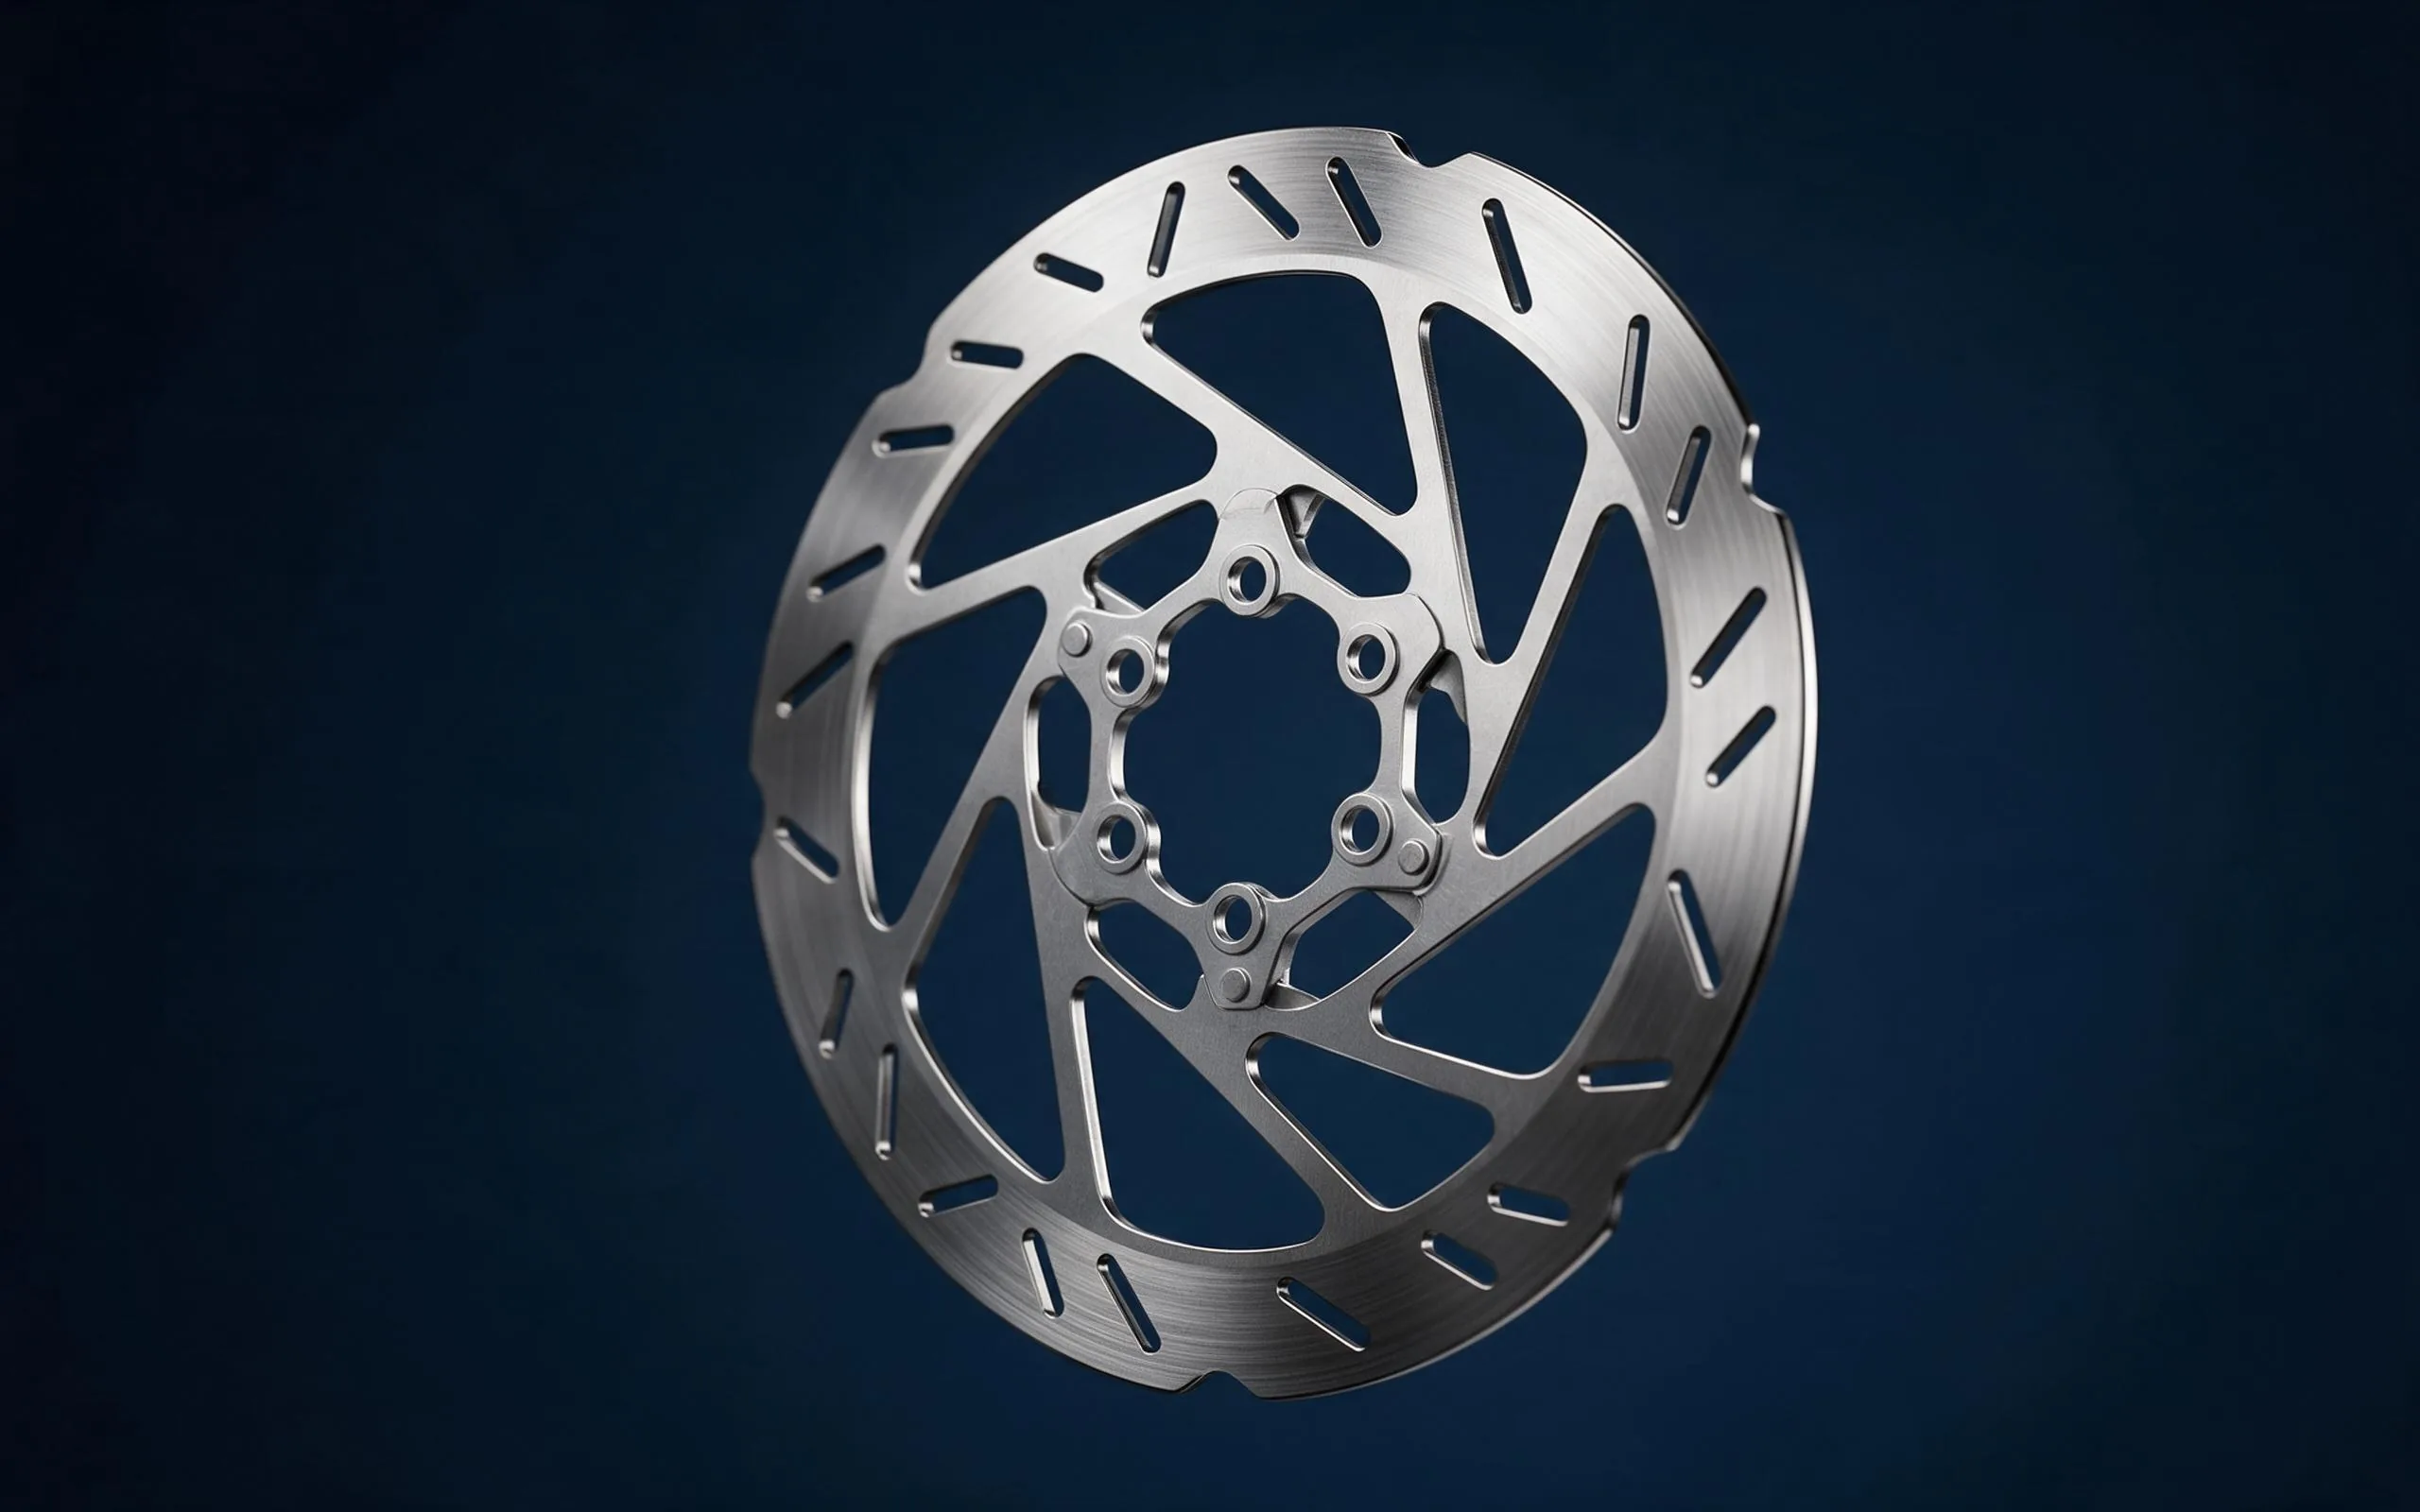
CNC machined bicycle disc brake rotor

Disc Rotors & Front Brake Disc Rotors

6-Bolt / Center-Lock

We review disc rotors & front brake disc rotors against the drawing to confirm process fit and inspection scope.

CharacteristicToleranceVerification
Flatness (both faces)As specified in the drawing / agreed scopeAs specified in the drawing / agreed scope
Thickness variationPer drawingInspection method agreed for project
Lateral runoutAs specified in the drawing / agreed scopeInspection method agreed for project
Cooling slot positionPer drawingInspection method agreed for project

Material is selected by duty cycle:

MaterialTypical UsePost-Machining
410 stainlessStandard road and gravel rotorsHarden, temper, surface grind
420 stainlessHeavy-duty MTB and e-bike rotorsHarden, temper, surface grind
7075-T6 aluminum (carrier)Floating-rotor carriers and spider armsType III hard anodize
410 / 420 SS Per drawing / agreed scope Heat Treated
Quote Rotors

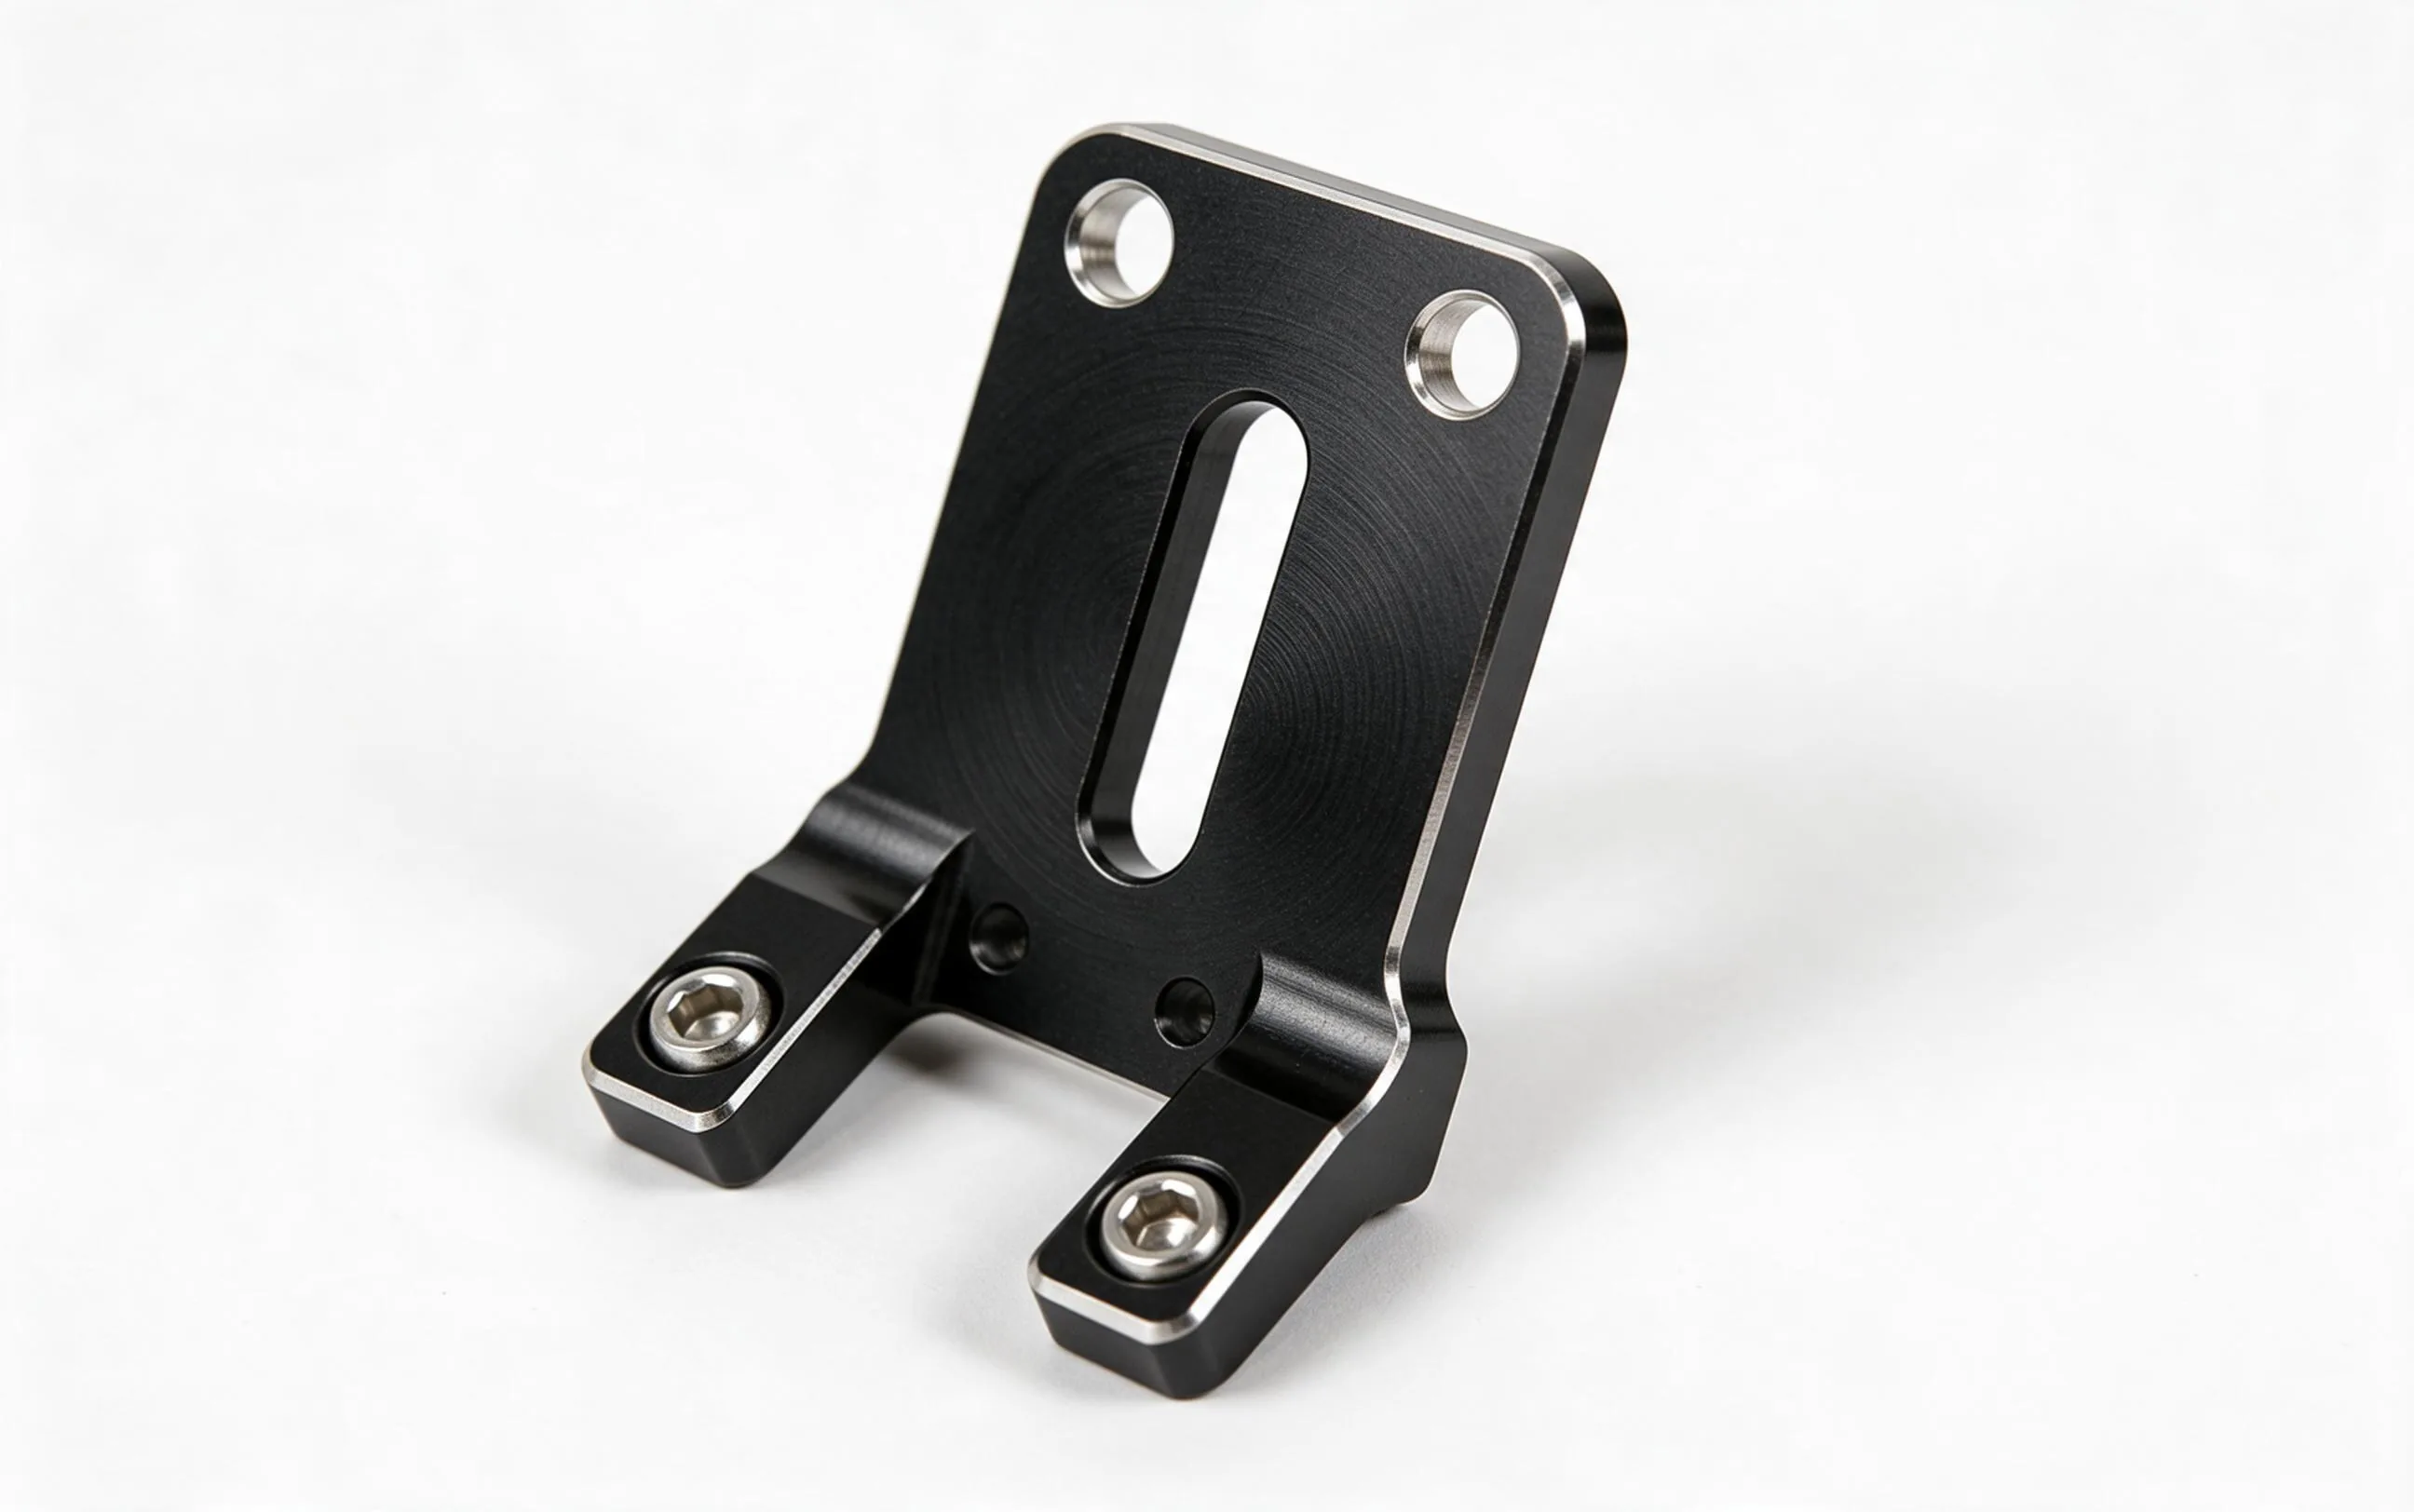
Brake Adapters & Mounts

IS / Post Mount
7075-T6 3B thread fit per drawing Hard Anodize
Quote Adapters
CNC machined bicycle brake adapter

Component Views from the Case

Real-world braking components machined for OEMs and aftermarket brands.

See More Brake Parts

Material and Process Decisions

7075-T6 aluminum for brake calipers

7075-T6 Aluminum

High strength for caliper bodies, adapters, and levers. Hard anodized for wear and corrosion resistance.

6061-T6 aluminum for master cylinders

6061-T6 Aluminum

Excellent machinability and corrosion resistance. Ideal for master cylinders and pistons.

Stainless steel for brake rotors

410 / 420 Stainless

Hardenable martensitic stainless for rotors. Heat-treated for wear resistance and flatness stability.

Titanium for lightweight brake hardware

Ti-6Al-4V

Lightweight hardware, bolts, and mounting pins with superior corrosion resistance.

Explore All Materials

Part Specifications and Acceptance Criteria

Typical tolerances and tests for bicycle brake parts.

ComponentCritical DimensionTest / Finish
Disc Brake CaliperPiston bore Fit requirements per drawing, seal groove Per drawingAs specified in the drawing / agreed scope
Master CylinderBore diameter Per drawingAs specified in the drawing / agreed scope
Brake LeverPivot bore requirements per drawingImpact test, Type II anodize
Disc RotorAs specified in the drawing / agreed scopeHeat treat, surface grind
Adapter / MountMounting face flatness Per drawingHard anodize, thread gauge
PistonOD Per drawingCeramic coat, seal fit test
Request Spec Review

Need a Custom Brake Component Not Listed Here?

We regularly machine banjo fittings, bleed screws, pad retention pins, and hose couplings for hydraulic brake systems. Start a project inquiryβ€”we prepare quotations within two business days after receiving complete drawings and project requirements.

Start a Project Inquiry

Frequently Asked Questions

The part geometry, material, feature access, and quantity determine the suitable machining route. Feasibility and inspection scope are reviewed from the drawing before quotation.

Tolerance and fit requirements are reviewed against the supplied drawing. Feasibility depends on geometry, material, machining process, and agreed inspection scope.

Any pressure, leak, or functional test requirement is reviewed against the customer specification. Test method, acceptance criteria, and records are included only when agreed for the project.

Material grade is considered against part function, operating conditions, and drawing requirements. Availability, finish options, and any requested material records are confirmed during quotation.

Material grade is considered against part function, operating conditions, and drawing requirements. Availability, finish options, and any requested material records are confirmed during quotation.

Finish options are reviewed against the material, operating environment, and drawing. Availability, acceptance criteria, and any external processing are confirmed in the project scope.

The part geometry, material, feature access, and quantity determine the suitable machining route. Feasibility and inspection scope are reviewed from the drawing before quotation.

Manufacturing lead time is confirmed after reviewing material availability, machining process, finish, and quantity. Quotation timing is two business days after complete drawings and requirements are received.

Ask Us Your Specific Question

Stopping Power, Engineered to Trust

The drawing defines the datums and fit criteria for the brake component; inspection scope is agreed for the project.

Get Your quotation