Bicycle Drivetrain Components CNC Machining Case Study

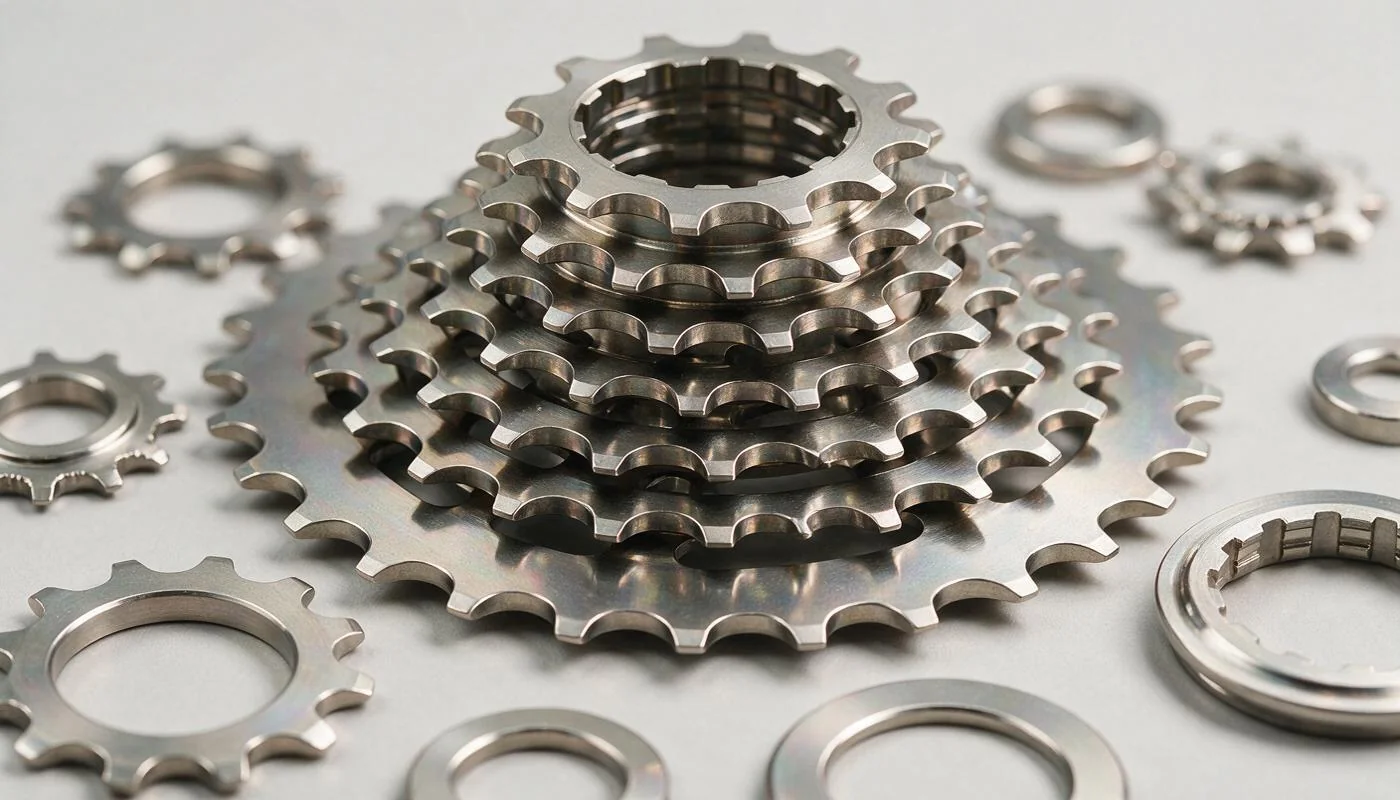
This bicycle drivetrain case follows a chainring and crank interface from drawing review through machining and inspection planning. The focus is on the fit between tooth geometry, mounting pattern and the adjoining drivetrain components.

Get Your Drivetrain Quote
Why Precision Matters
Case Brief: Part Function and Requirements

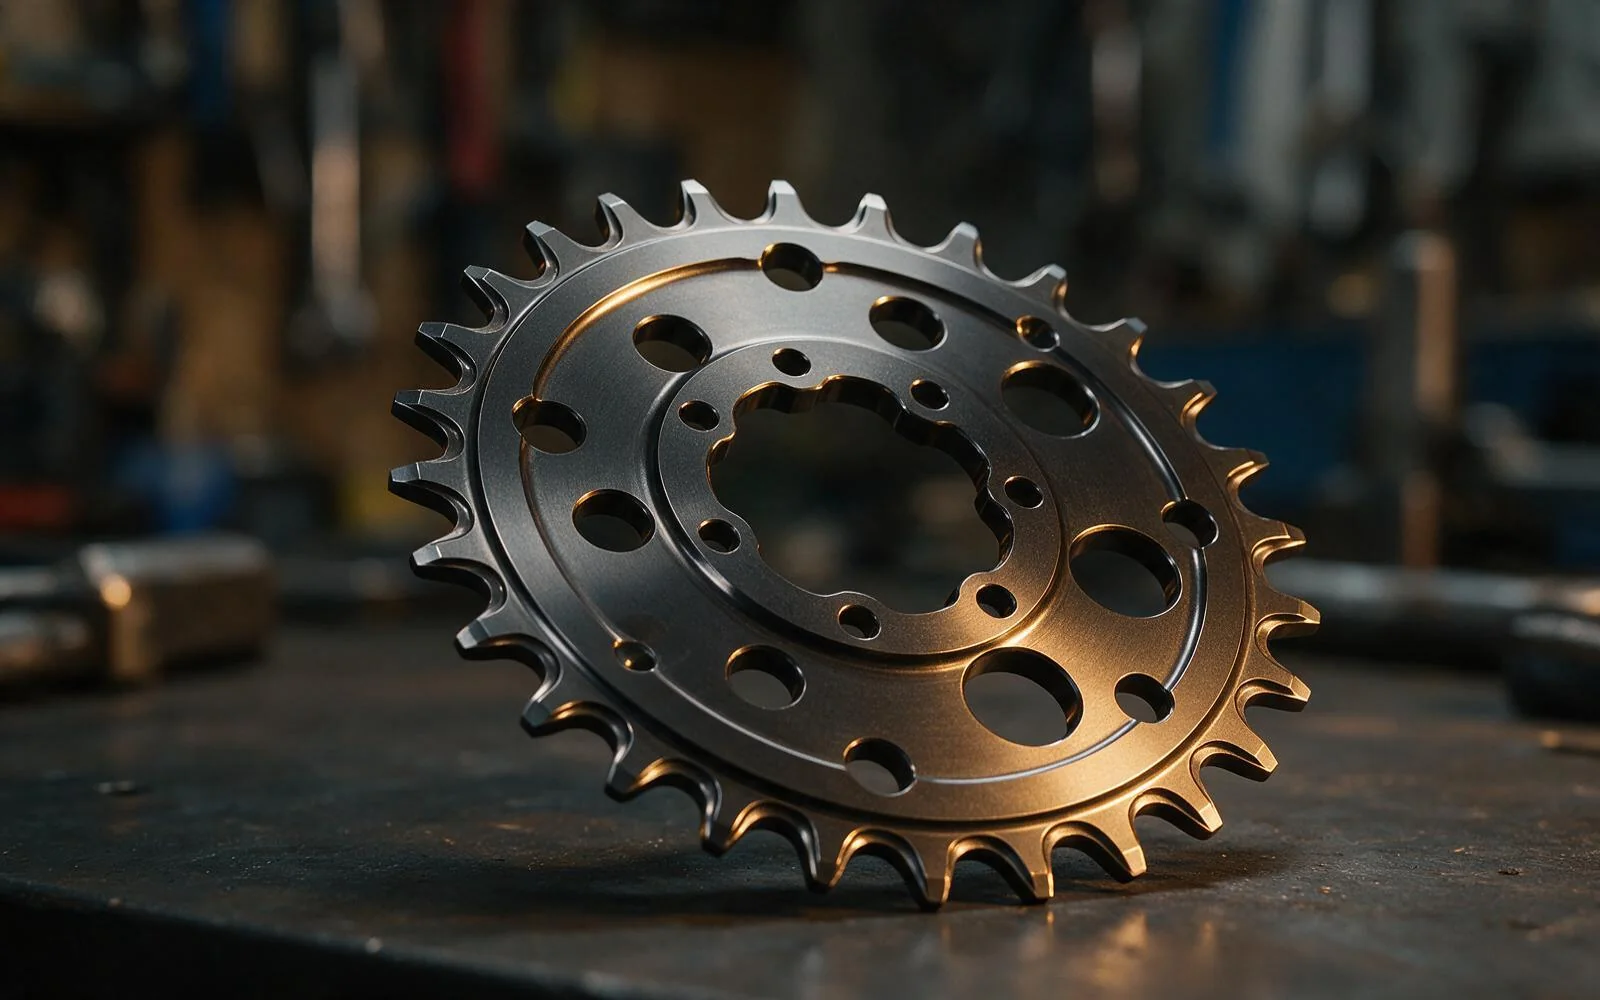
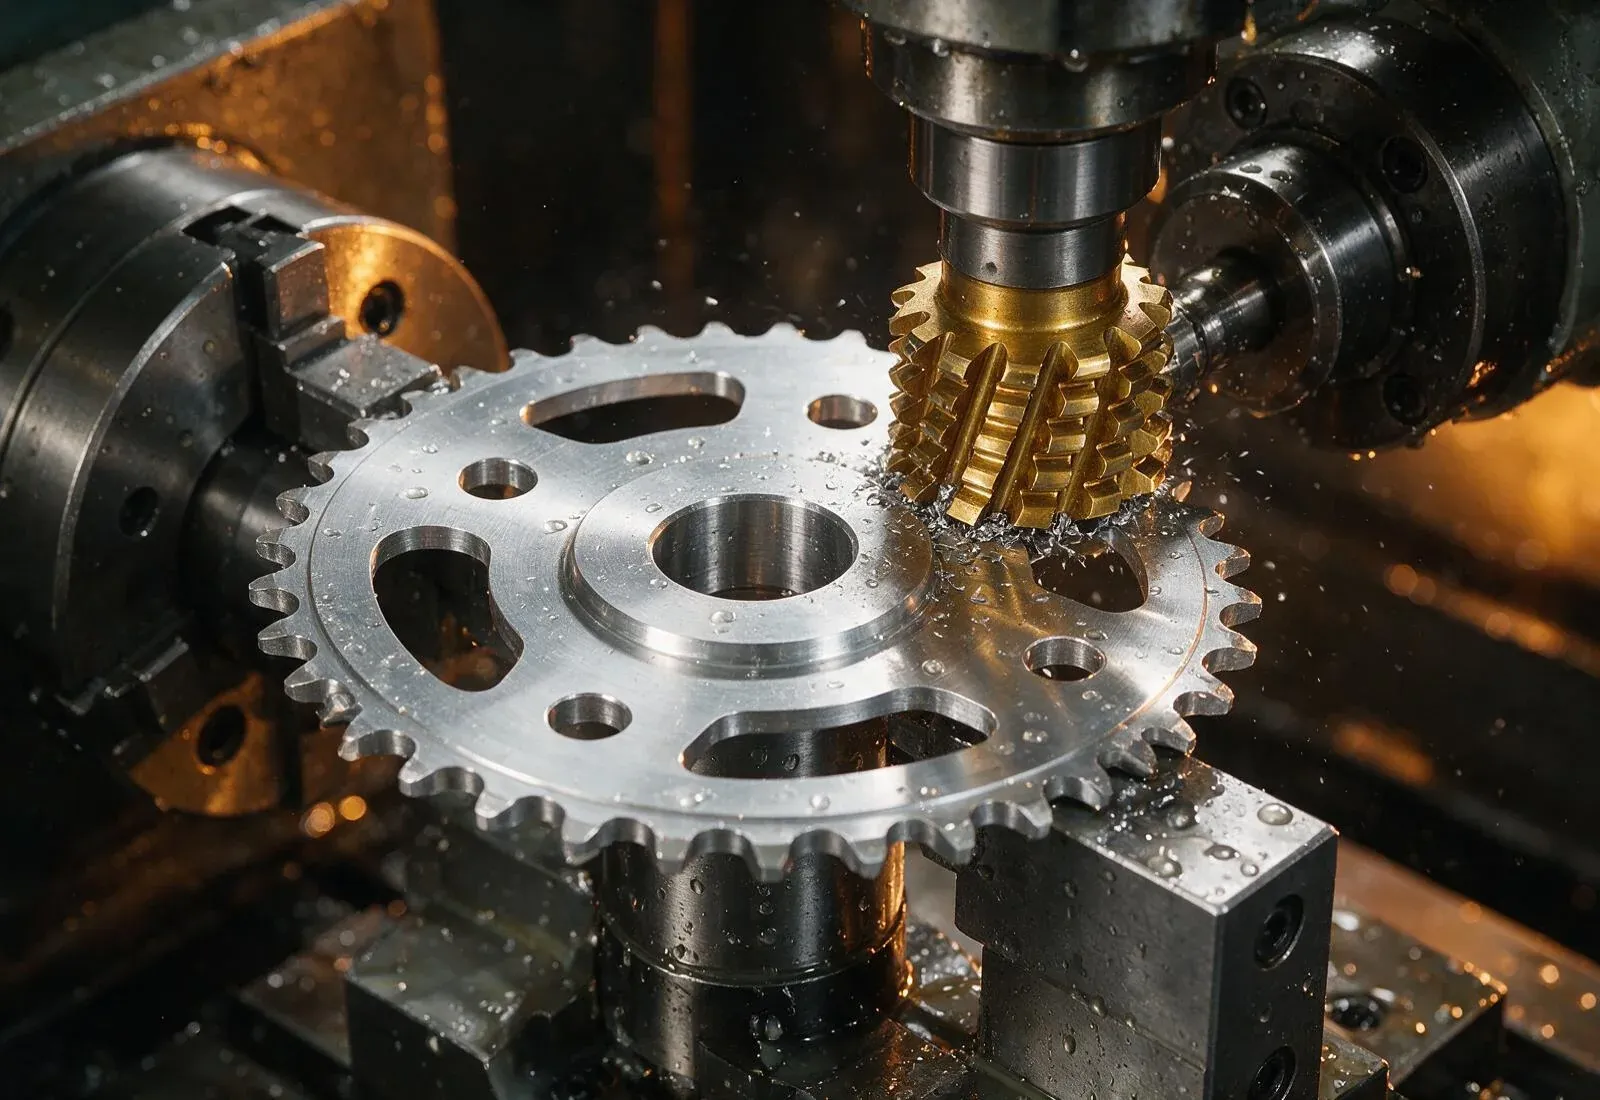
CNC gear hobbing a 7075-T6 bicycle chainring on a 5-axis machine 7075-T6 Β· Chainring Hobbing

The case centers on bicycle drivetrain parts where a chainring, spider or crank feature must align with neighboring components. Bicycle drivetrain components transfer motion through a linked system, so tooth profile, bore location and mounting geometry are reviewed as a set.

The machining plan ties the workholding datum to the mounting interface, then identifies which tooth and bore features need inspection. Parts of a bicycle drivetrain vary by design, so material, finish and acceptance criteria are taken from the project drawing rather than assumed from a generic setup.

Road & Gravel Mountain & Enduro BMX & Track E-Bike Torque Gear Hobbing 5-Axis Milling
Case Components and Machining Focus

Inspection method, acceptance criteria, and requested records are agreed for the part and project scope.

  1. Per drawing / agreed scope
  2. For drivetrain, datum, feature, and inspection requirements are taken from the part drawing and agreed project scope.
  3. For drivetrain, datum, feature, and inspection requirements are taken from the part drawing and agreed project scope.
  4. 04

    Derailleur Hangers

    7075-T6; machined to exact frame-dropout geometry, M5 threads Fit requirements per drawing.

  5. For derailleur hangers, datum, feature, and inspection requirements are taken from the part drawing and agreed project scope.
  6. 06

    Spider Adapters & Chain Guides

    7075-T6 with Type III hard anodizing for wear-critical interfaces.

Inspection method, acceptance criteria, and requested records are agreed for the part and project scope.

Request a Component Quote

Component Engineering Deep-Dives

Detailed specifications for mission-critical drivetrain parts.

Bicycle chainring tooth profile CNC machined

Chainrings

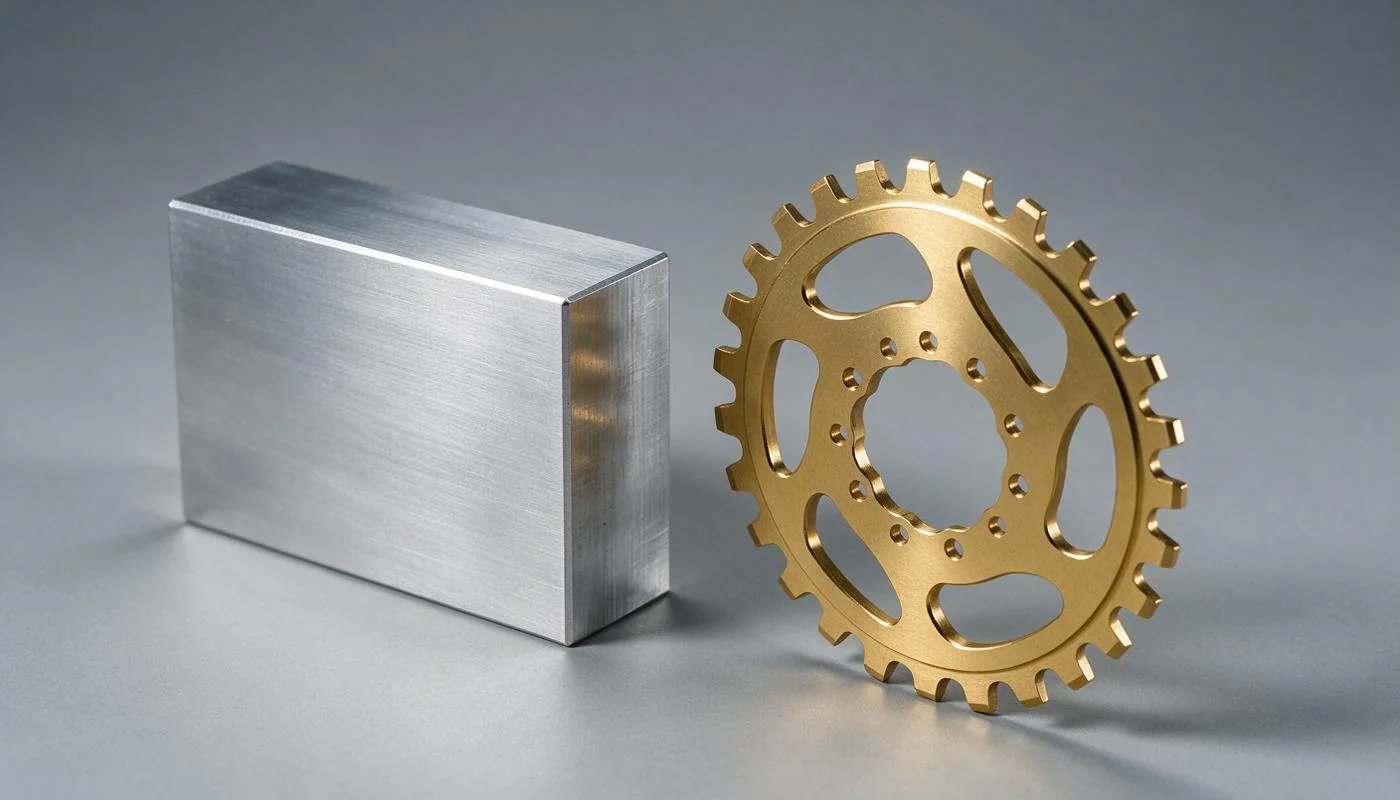
According to our CNC machining knowledge base, gear hobbing is a specialty CNC machining process used to create gear teeth by progressively cutting them into a cylindrical piece of material using a cutting tool called a hob. For bicycle chainrings, hobbing is effective for achieving accurate tooth profiles.

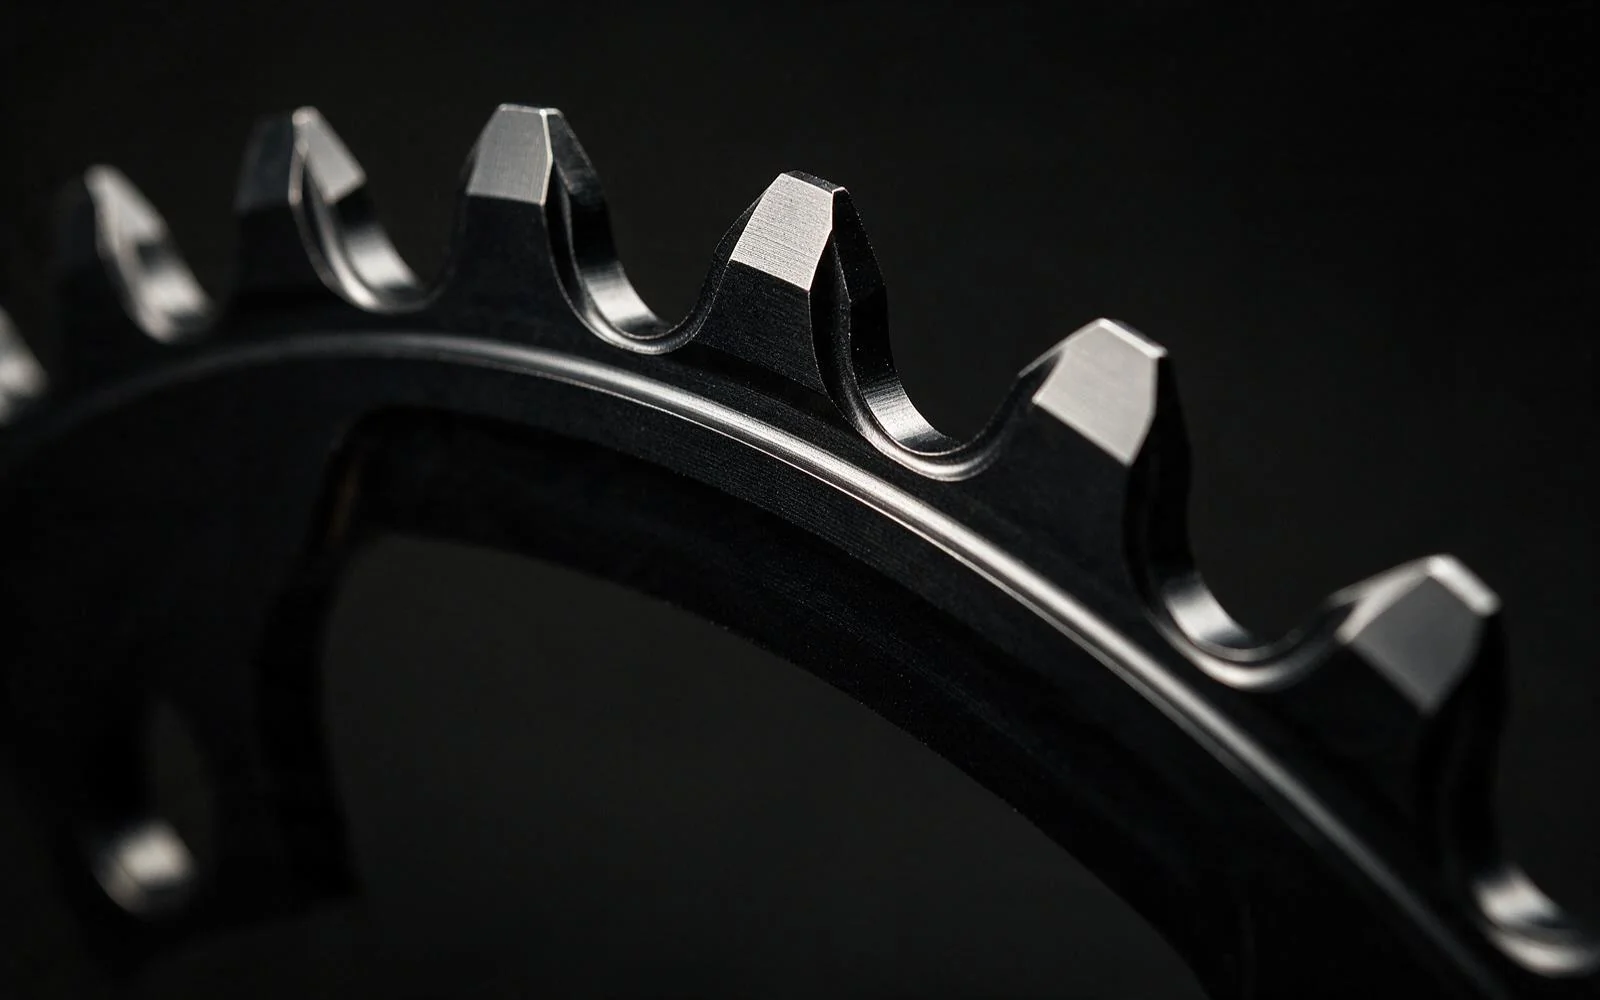
  • Narrow-wide tooth profiles for chain retention
  • Oval (OCP) and round options available
  • BCD and direct-mount interfaces
  • Per drawing / agreed scope
Quote Chainrings

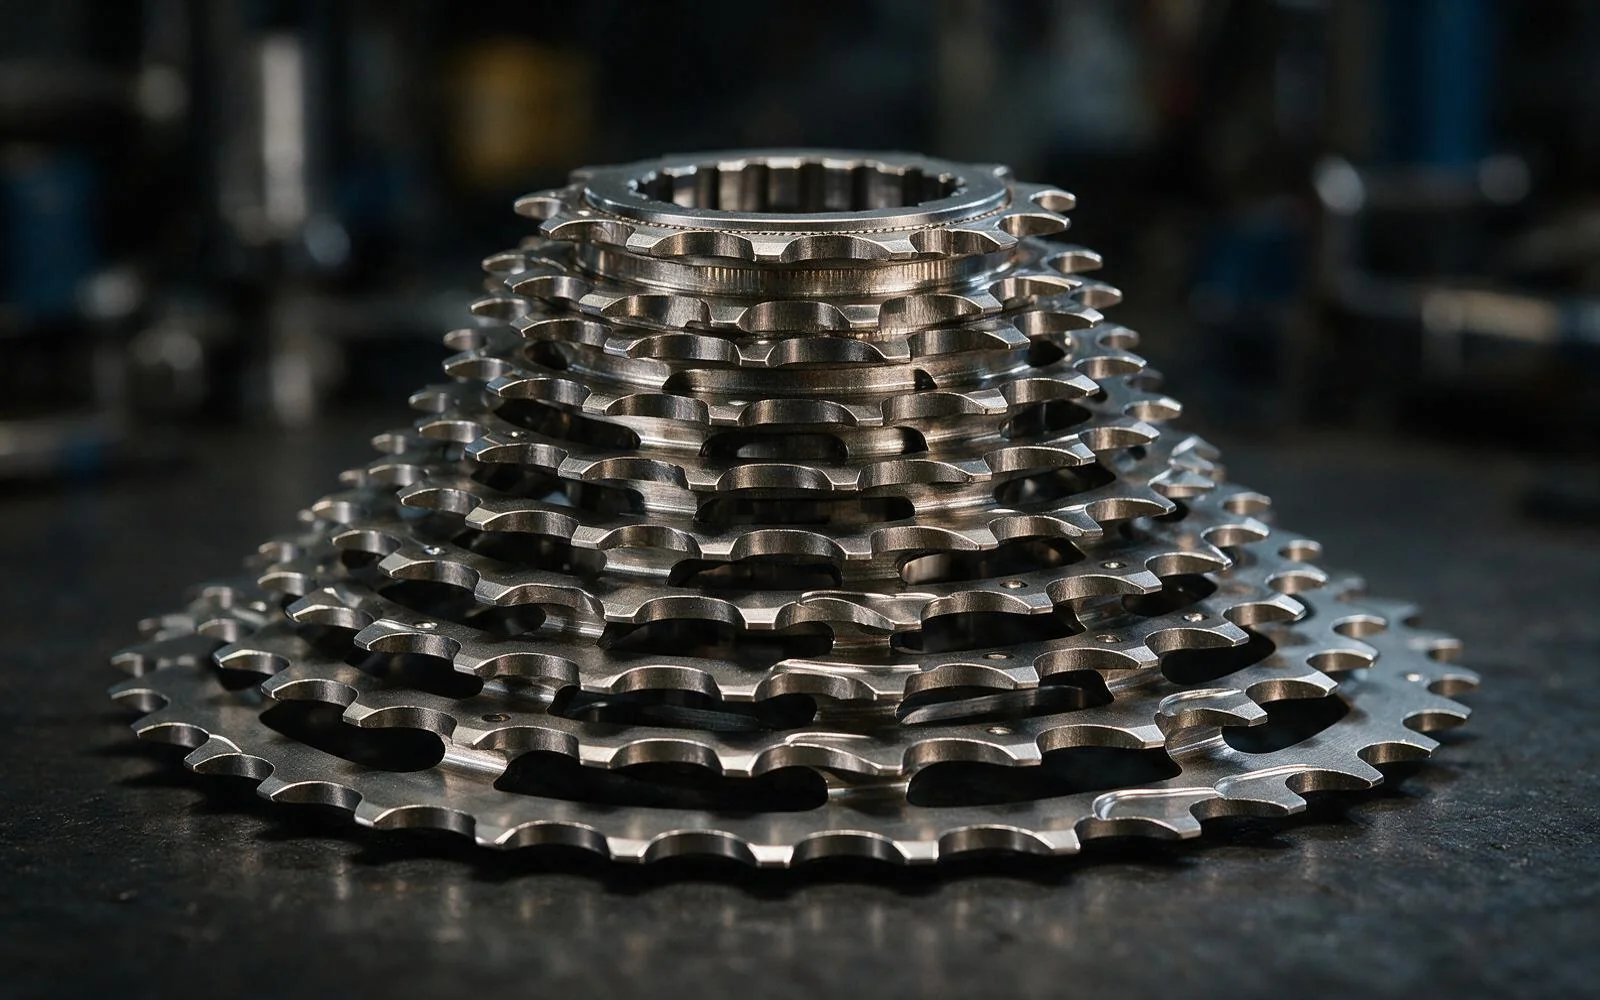
Cassettes

The drawing defines the datums and fit criteria for cassettes; inspection scope is agreed for the project.

  • Steel, aluminum, or titanium cogs
  • For cassettes, datum, feature, and inspection requirements are taken from the part drawing and agreed project scope.
  • Compatible with 10/11/12-speed systems
  • Nitriding or hard anodizing available
Quote Cassettes
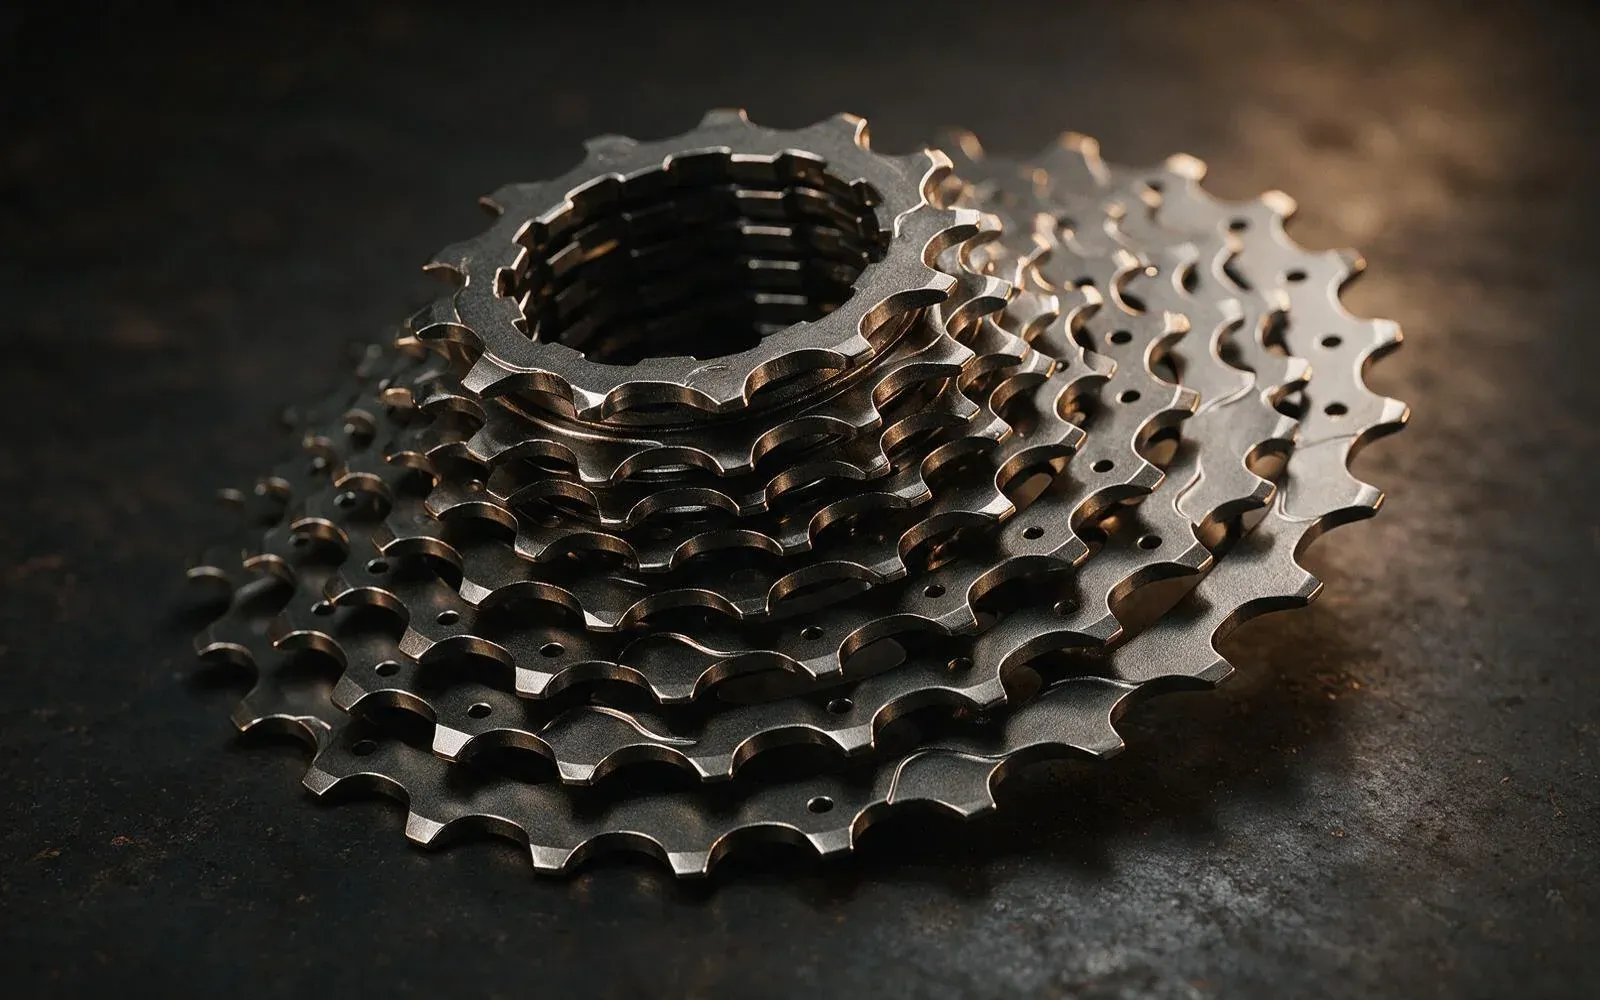
Bicycle cassette shift ramps CNC machined
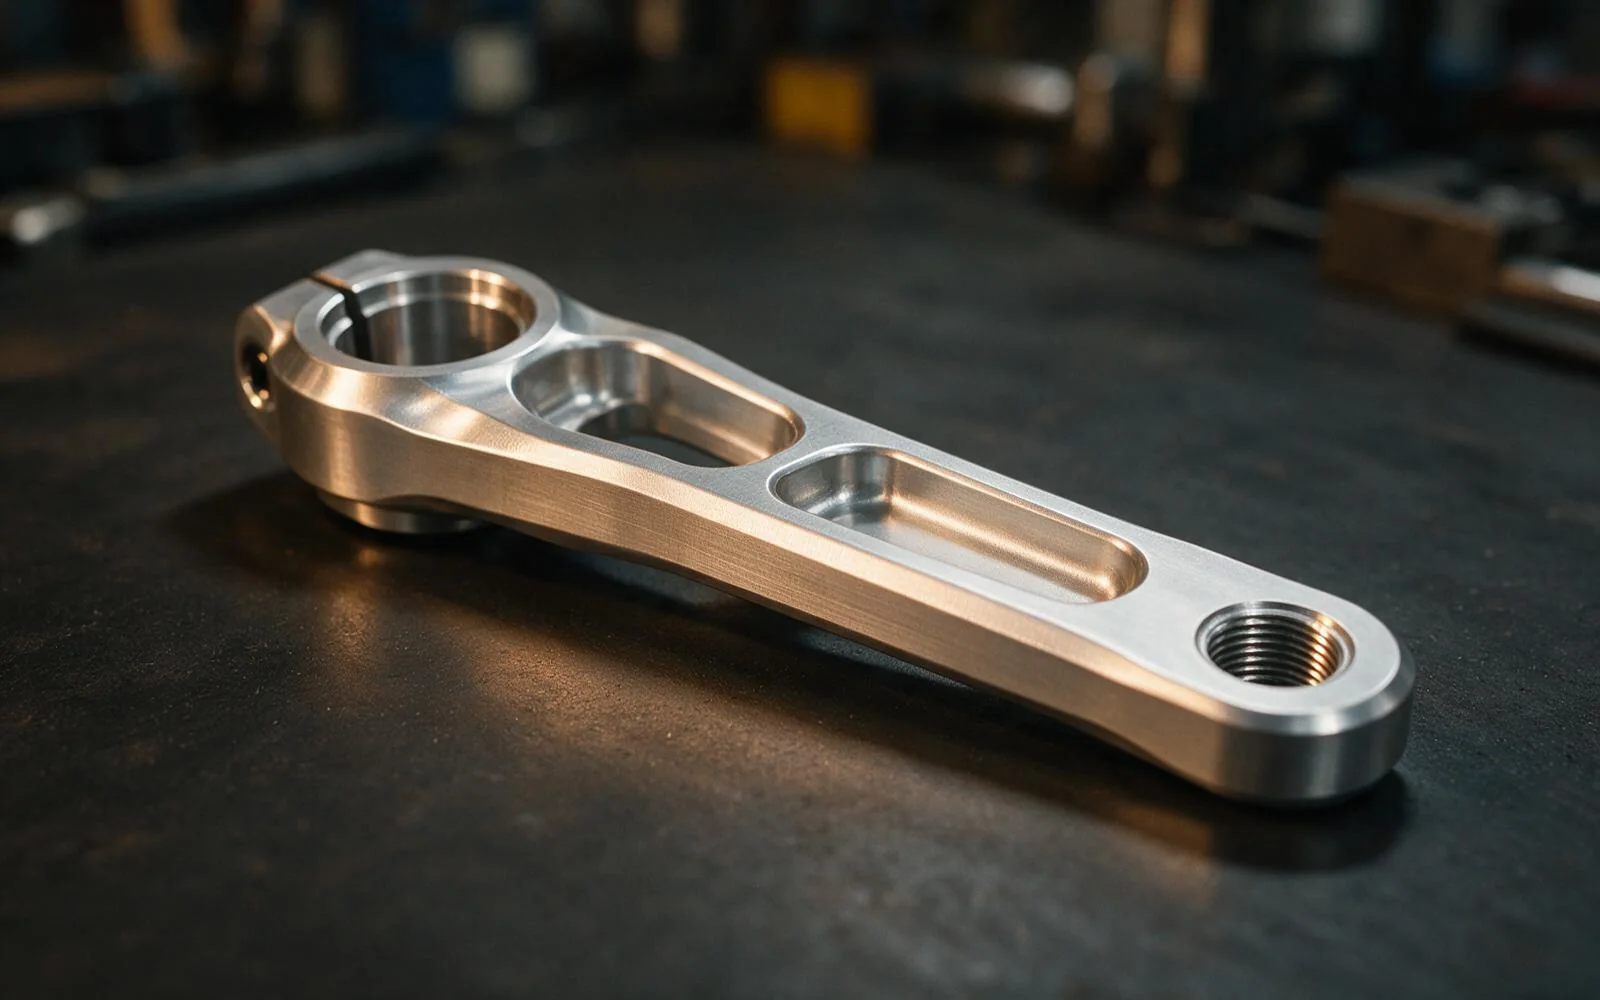
Bicycle crank arm CNC machined

Crank Arms & Spiders

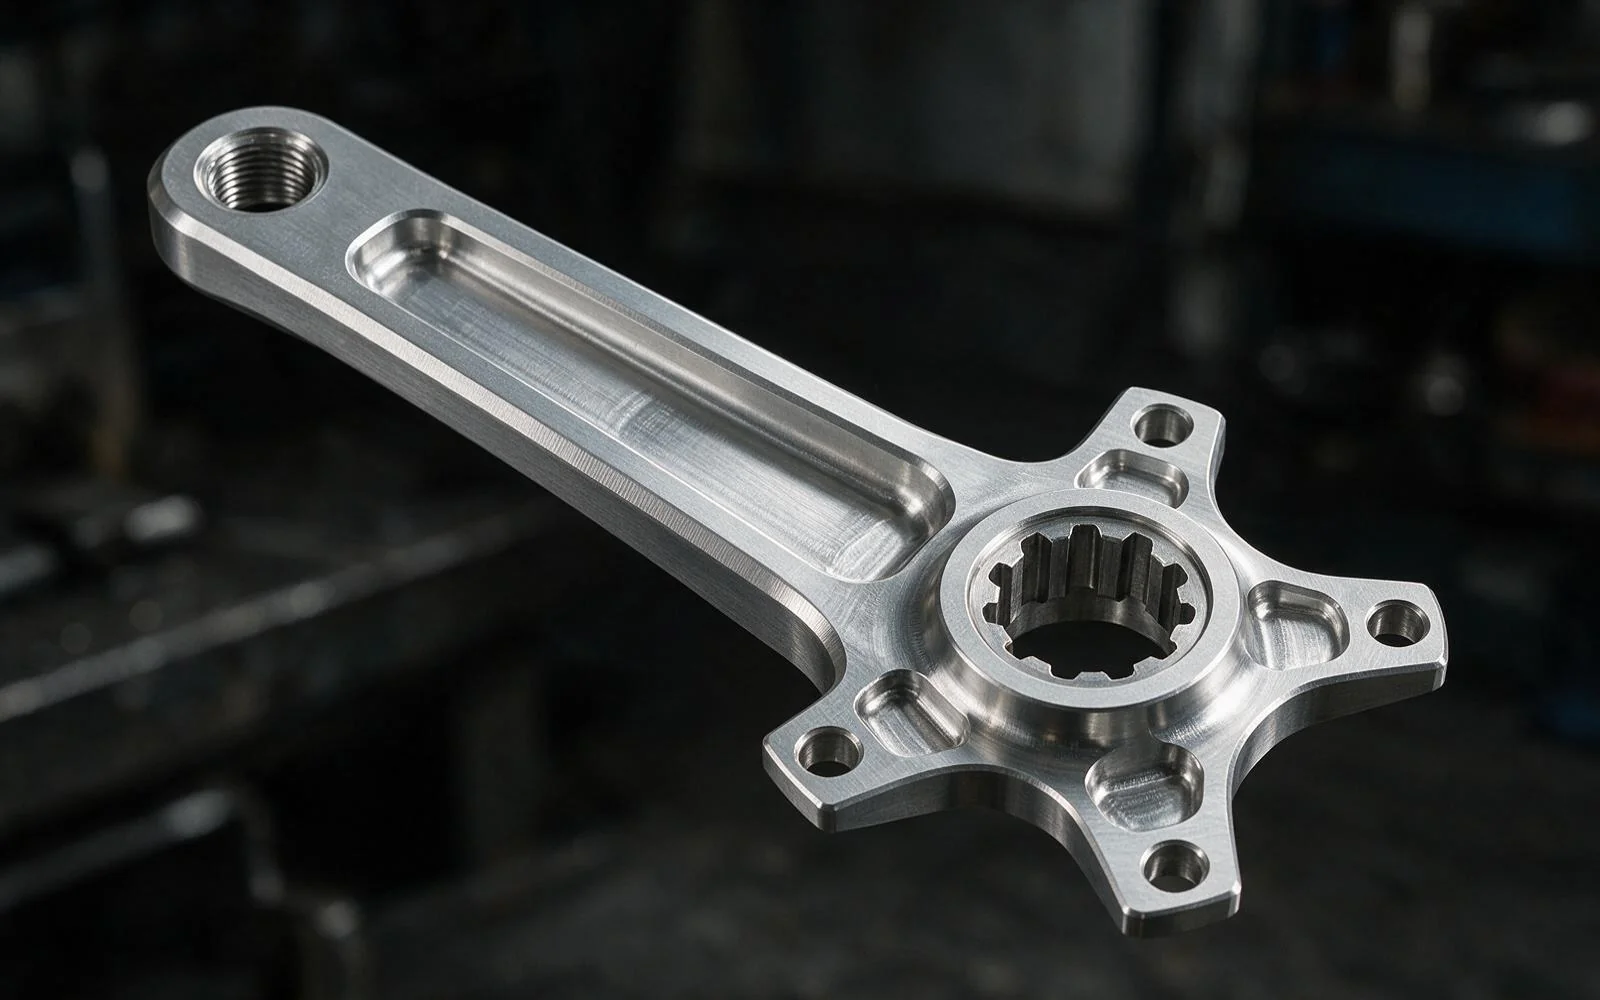
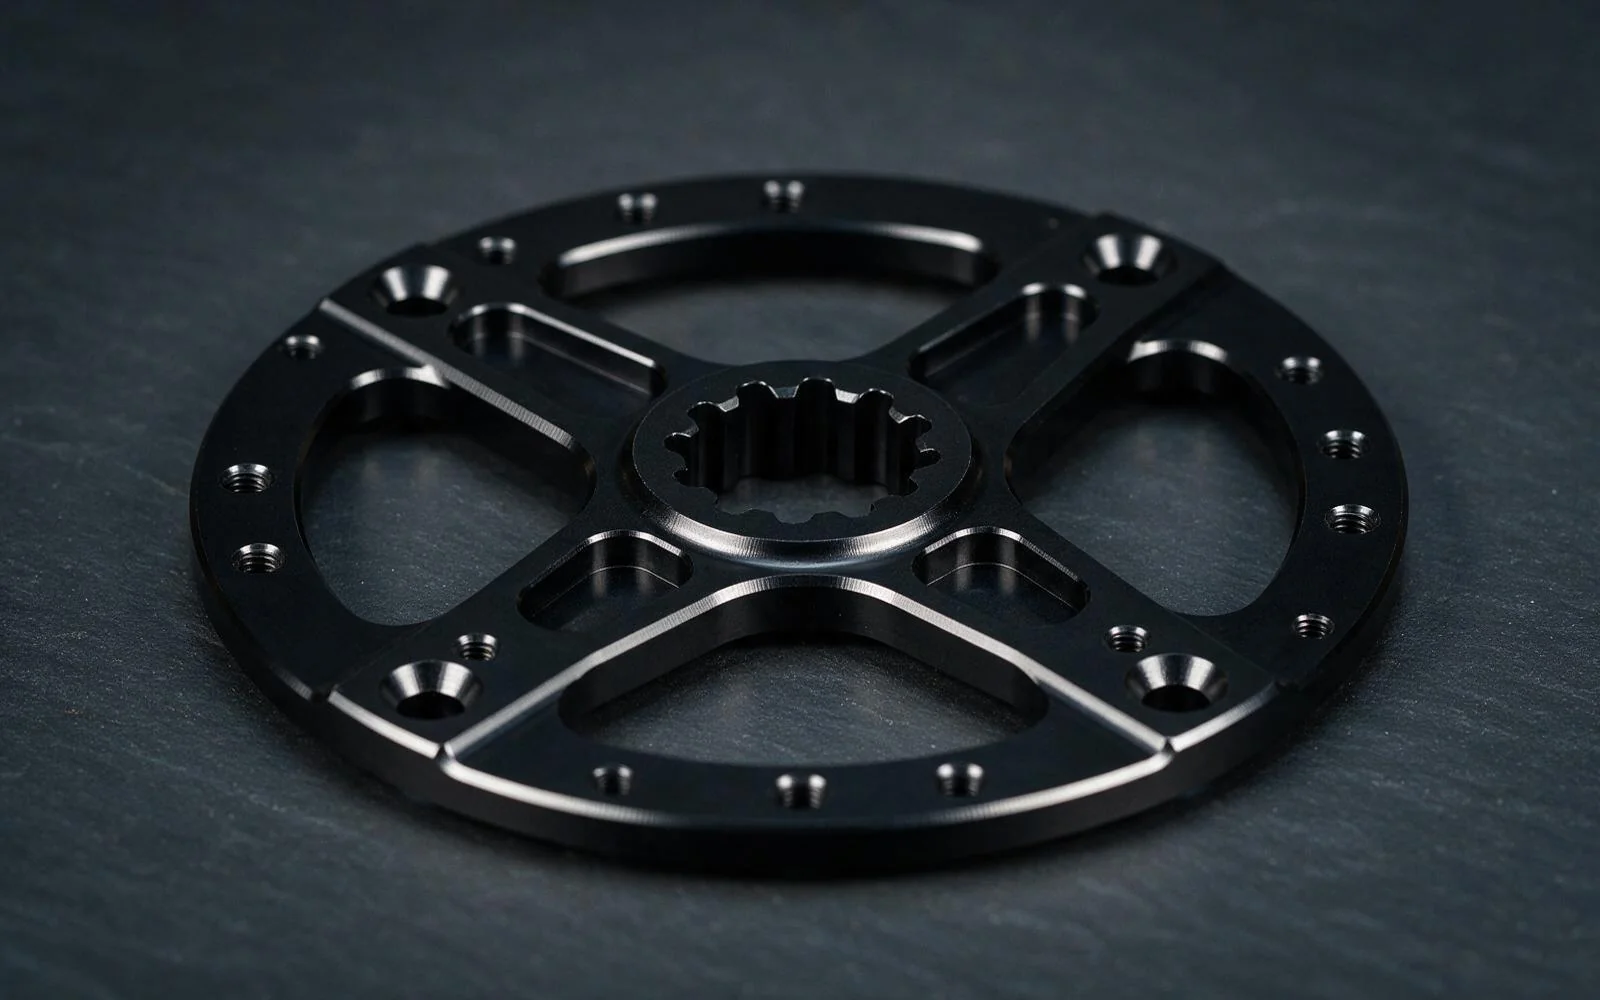
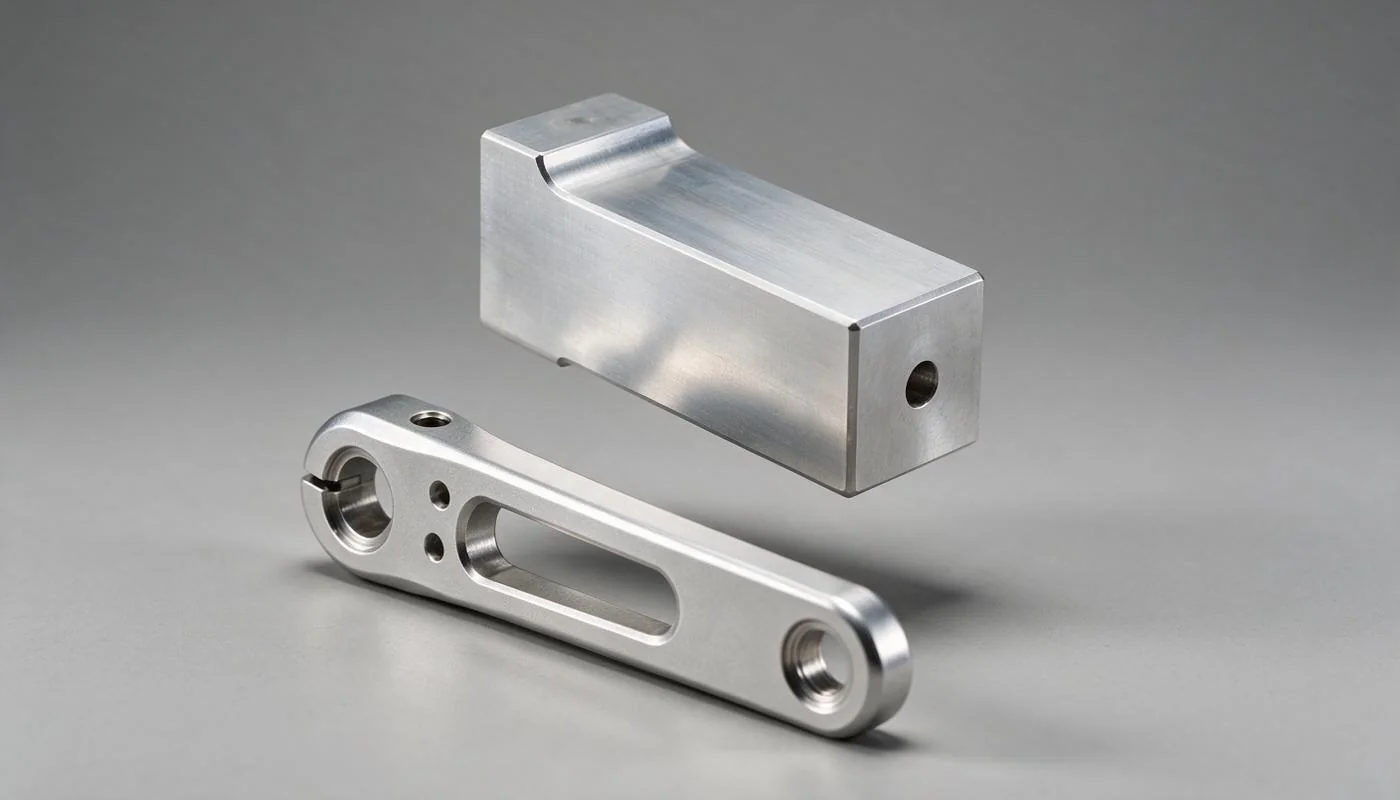
Crank arms transfer rider torque to the chainring. We machine forged blanks and billet crank arms with precise BB interfaces, pedal thread bores, and spider bolt circles. According to our CNC machining knowledge base, 6061 is easier and quicker to machine than 7075 due to lower hardness, while 7075 offers higher strength for high-load applications.

  • Per drawing / agreed scope
  • Pedal thread bores to meet fit requirements on the drawing
  • 4-arm and 5-arm spider patterns
  • Fatigue-tested to ISO 4210
Quote Crank Arms

Derailleur Hangers

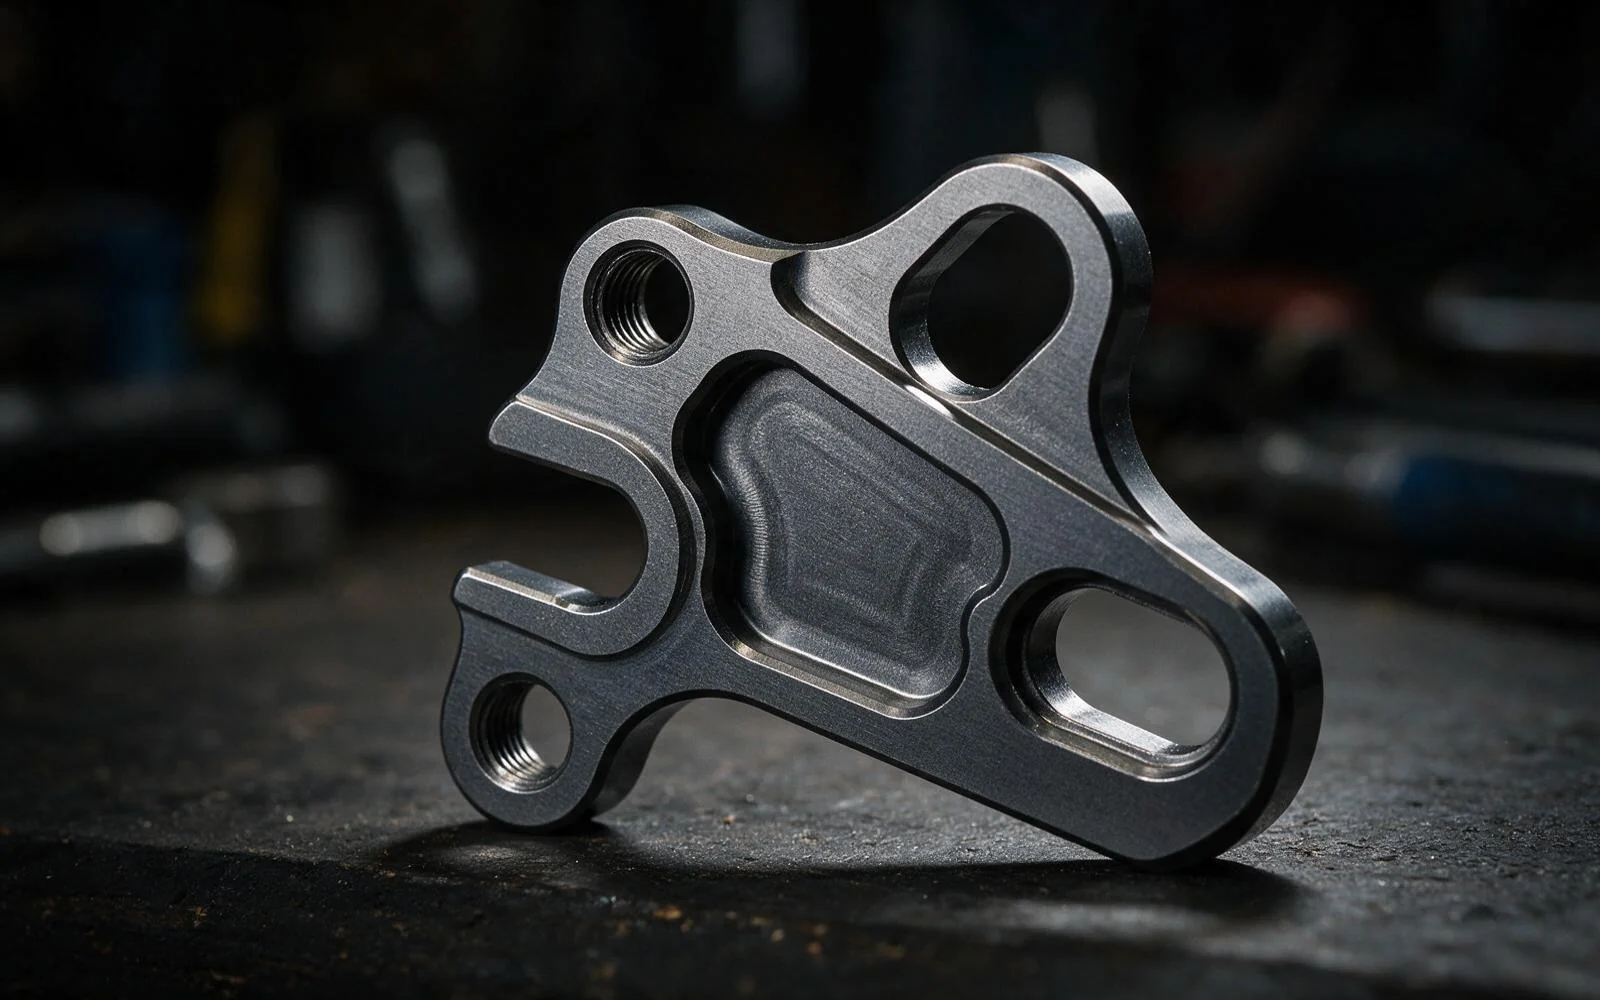
Derailleur hangers are sacrificial components that protect the frame and derailleur in a crash. We machine them from 7075-T6 aluminum to exact frame-dropout geometry, ensuring precise derailleur alignment for crisp shifting.

  • Frame-specific geometry matching
  • 7075-T6 for strength-to-weight
  • M5 threads to meet fit requirements on the drawing
  • Batch production for OEM spares
Quote Hangers
Bicycle derailleur hanger CNC machined
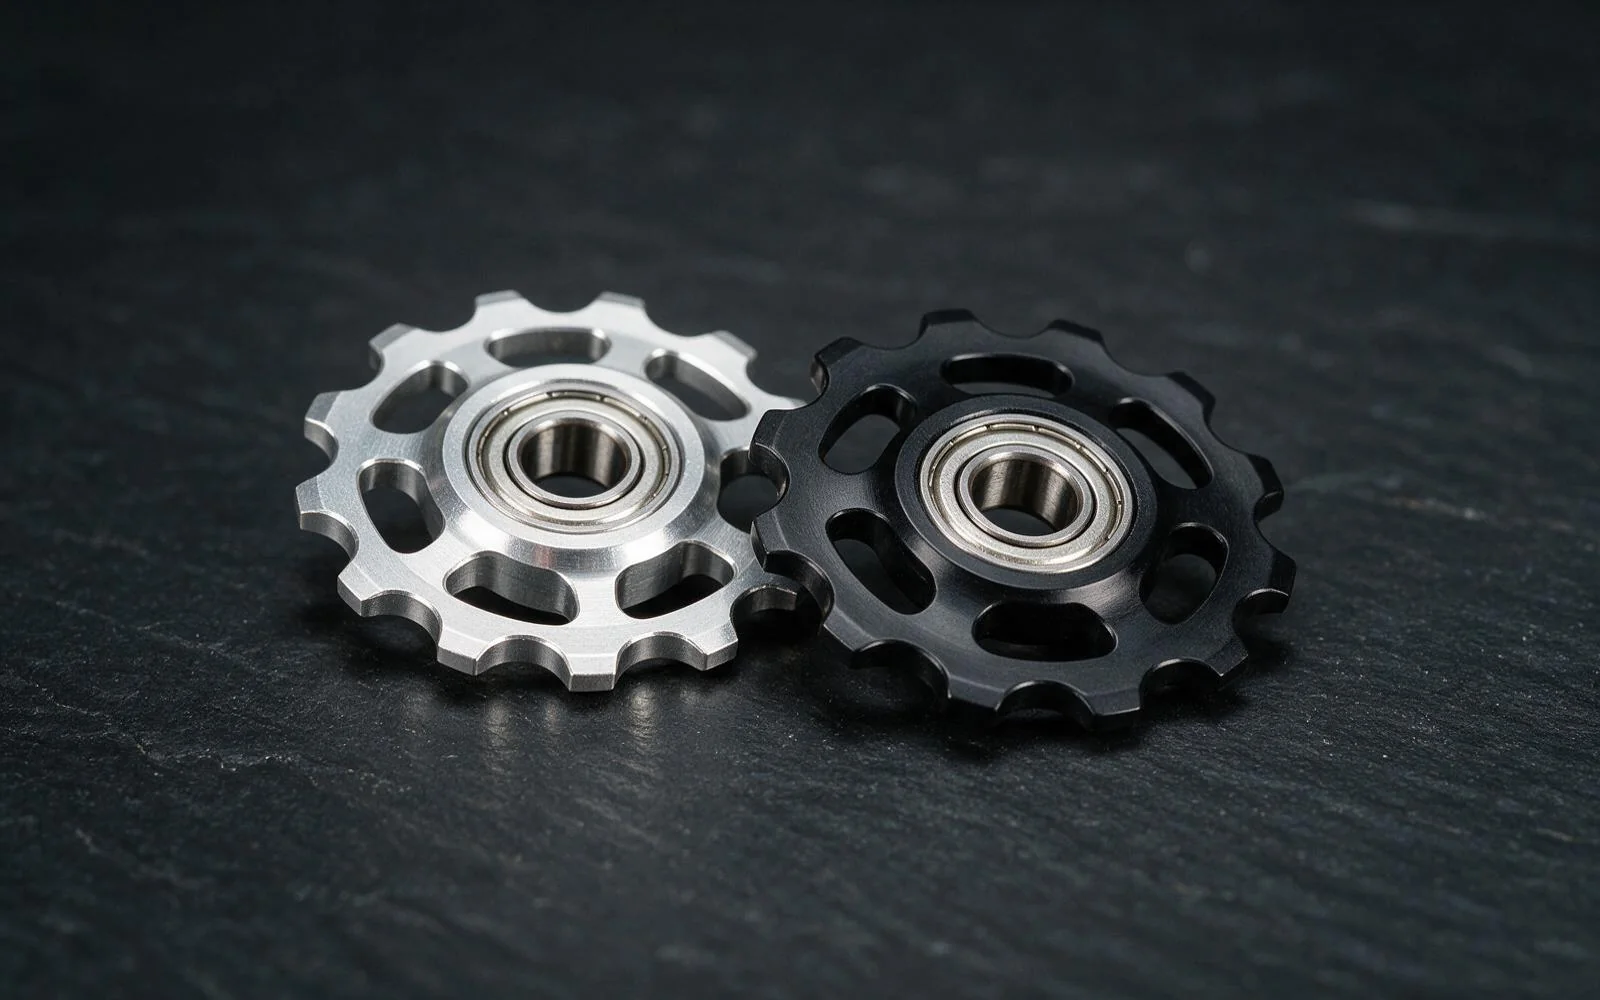
Bicycle derailleur pulley wheel CNC machined

Pulley Wheels & Cage Plates

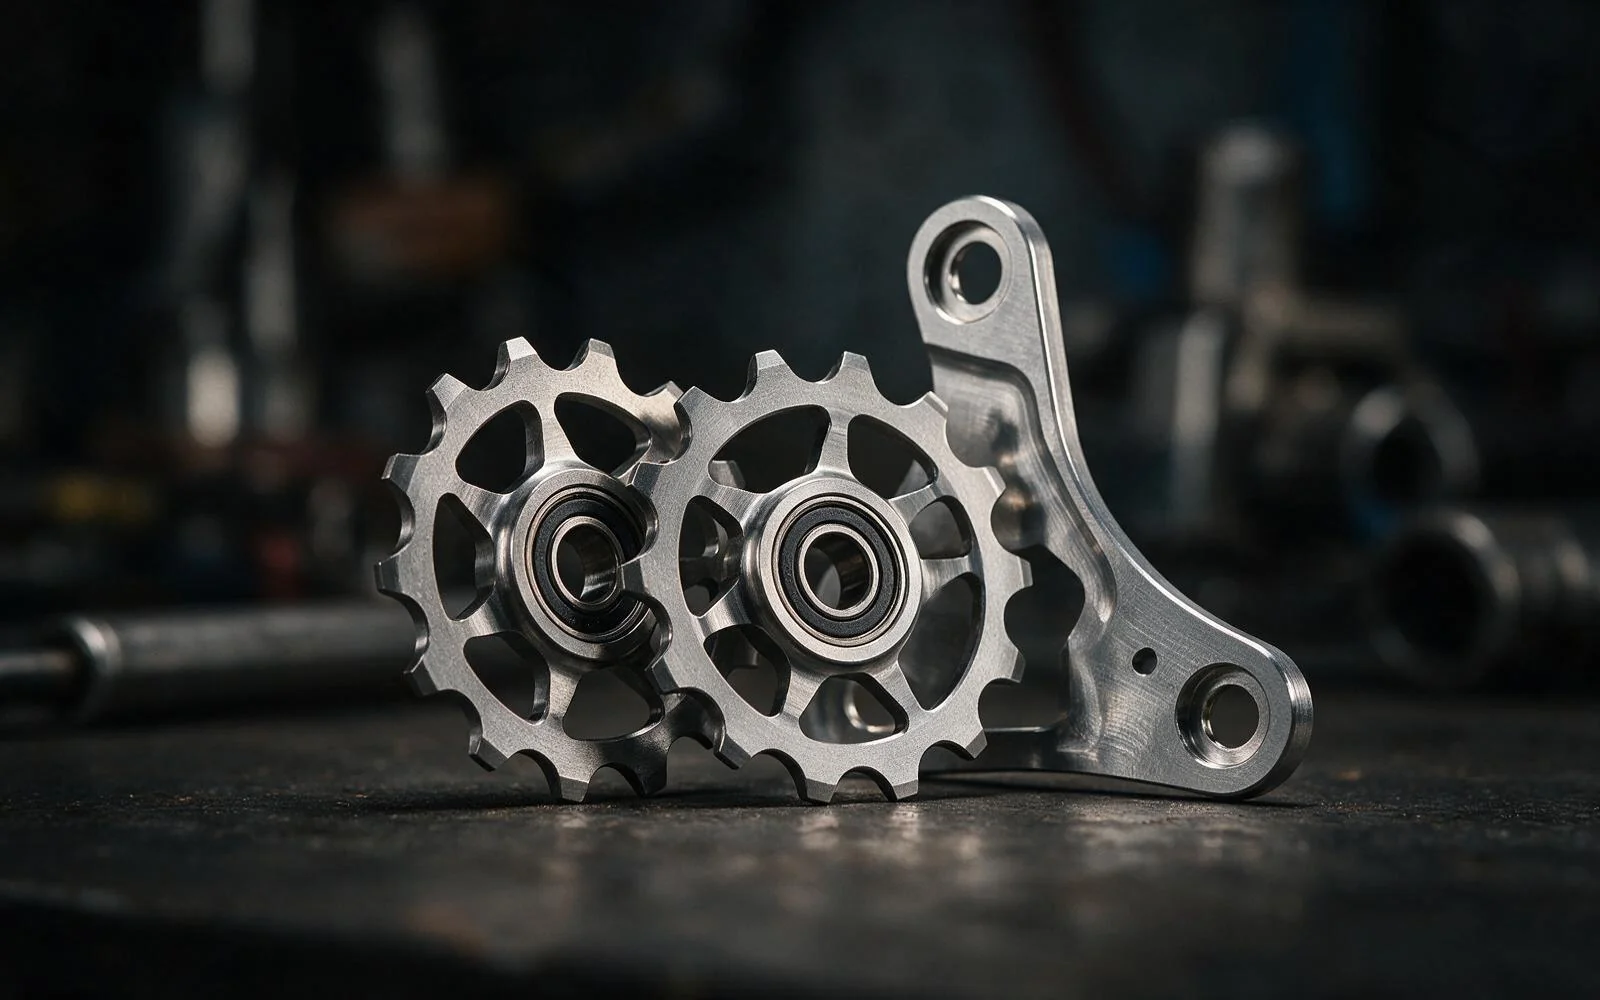
Pulley wheels guide the chain through the derailleur cage. We machine aluminum and Delrin pulleys with sealed-bearing bores and low-friction tooth profiles, plus cage plates with precise pivot and mounting holes.

  • For pulley wheels & cage plates, datum, feature, and inspection requirements are taken from the part drawing and agreed project scope.
  • Aluminum or Delrin construction
  • Cage plates with hardened pivot bores
  • Per drawing / agreed scope
Quote Pulleys

Case Components and Machining Focus

Real-world drivetrain components machined for OEM brands, race teams, and aftermarket builders.

Request a Component Quote

Bicycle Drivetrain Systems & Types We Support

From conventional multi-chainring setups to belt and chainless designs β€” each drivetrain bicycle architecture changes which surfaces carry load, and therefore how we machine them.

System Type
Typical Parts We Machine
Materials
Machining Challenge
1x (Single Chainring)
Narrow-wide chainrings, direct-mount spiders, chain guides
7075-T6, 6061-T6
Finish options are confirmed against the drawing and intended operating conditions.
Chain (2x / 3x)
Chainrings, cassette cogs, crank arms, derailleur hangers
7075-T6, hardened steel, Ti
Shift ramps and gates positioned to drawing requirements for gear engagement
Belt Drive
Front & rear pulleys (sprockets), belt tensioners, guides
7075-T6 with Type III anodize
Pulley tooth pitch and concentricity β€” an error in tooth pitch or concentricity can cause belt skip or premature wear
Chainless (Shaft / Gearbox)
Bevel & spur gears, gearbox housings, sealed shafts
7075-T6, hardened steel
Gear mesh and housing bore alignment drive efficiency; concentricity per drawing

Discuss your drivetrain part, materials, and finish requirements with our team. Drawing files can be shared through an agreed channel after initial contact. Start a project inquiry.

Material and Process Decisions

7075-T6 aluminum for chainrings

7075-T6 Aluminum

High strength comparable to many steels. Ideal for chainrings, hangers, and spider adapters.

6061-T6 aluminum for crank arms

6061-T6 Aluminum

Excellent machinability and weldability. Cost-effective choice for crank arms and cage plates.

Hardened steel for cassette cogs

Hardened Steel

Superior wear resistance for cassette cogs. Compatible with nitriding for extended life.

Titanium for lightweight cogs

Titanium

Lightweight and corrosion-resistant. Premium option for lightweight cassette cogs and hardware.

Explore All Materials

Surface Finishes for Durability & Aesthetics

Finish
Specification
Application
Hard Anodizing (Type III)
Per drawing / agreed finish scope
Chainrings, hangers, abrasion resistance
Decorative Anodizing (Type II)
Per drawing / agreed finish scope
Crank arms, cage plates, cosmetics
Nitriding
Per drawing / agreed finish scope
Steel cassette cogs, wear resistance
Powder Coating
UV-resistant, multiple colors
Crank arms, protective cosmetic layer
Passivation
Citric or nitric acid
Titanium and stainless components
Request Finish Samples

Need a Custom Drivetrain Component Not Listed Here?

We regularly machine chain guides, bash guards, chain stay protectors, and custom BCD adapters for boutique builders and OEMs. Start a project inquiryβ€”we prepare quotations within two business days after receiving complete drawings and project requirements.

Start a Project Inquiry

Frequently Asked Questions

The part geometry, material, feature access, and quantity determine the suitable machining route. Feasibility and inspection scope are reviewed from the drawing before quotation.

The part geometry, material, feature access, and quantity determine the suitable machining route. Feasibility and inspection scope are reviewed from the drawing before quotation.

Material grade is considered against part function, operating conditions, and drawing requirements. Availability, finish options, and any requested material records are confirmed during quotation.

The part geometry, material, feature access, and quantity determine the suitable machining route. Feasibility and inspection scope are reviewed from the drawing before quotation.

Finish options are reviewed against the material, operating environment, and drawing. Availability, acceptance criteria, and any external processing are confirmed in the project scope.

Tolerance and fit requirements are reviewed against the supplied drawing. Feasibility depends on geometry, material, machining process, and agreed inspection scope.

Requested quantity and production stages are reviewed against the part geometry, material, and process. Capacity and manufacturing lead time are confirmed for the agreed project scope.

Manufacturing lead time is confirmed after reviewing material availability, machining process, finish, and quantity. Quotation timing is two business days after complete drawings and requirements are received.

Ask Us Your Specific Question

Power Transfer, Perfected

The drawing defines the datums and fit criteria for the drivetrain component; inspection scope is agreed for the project.

Get Your quotation